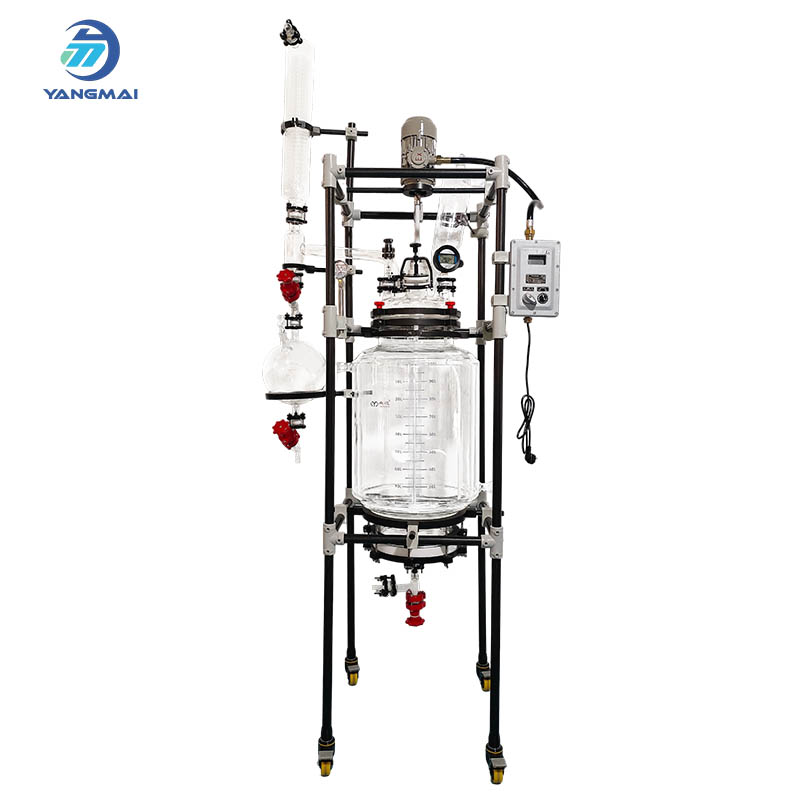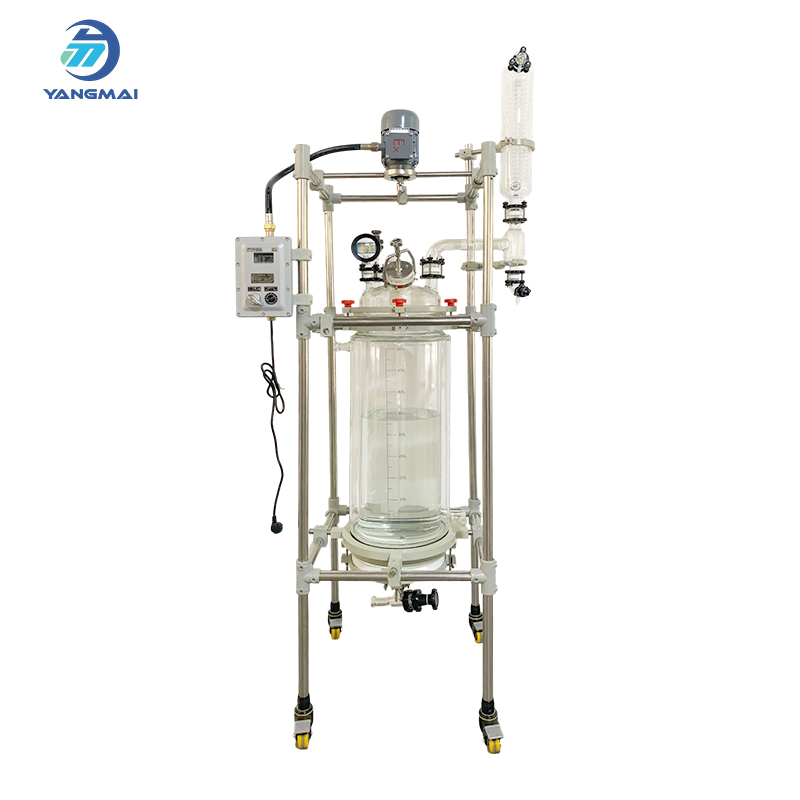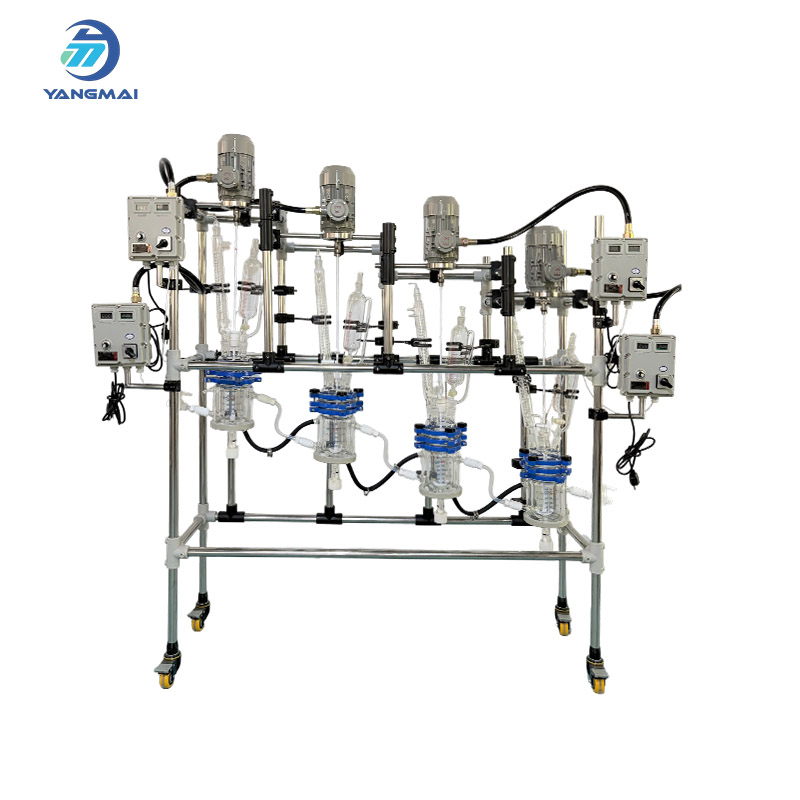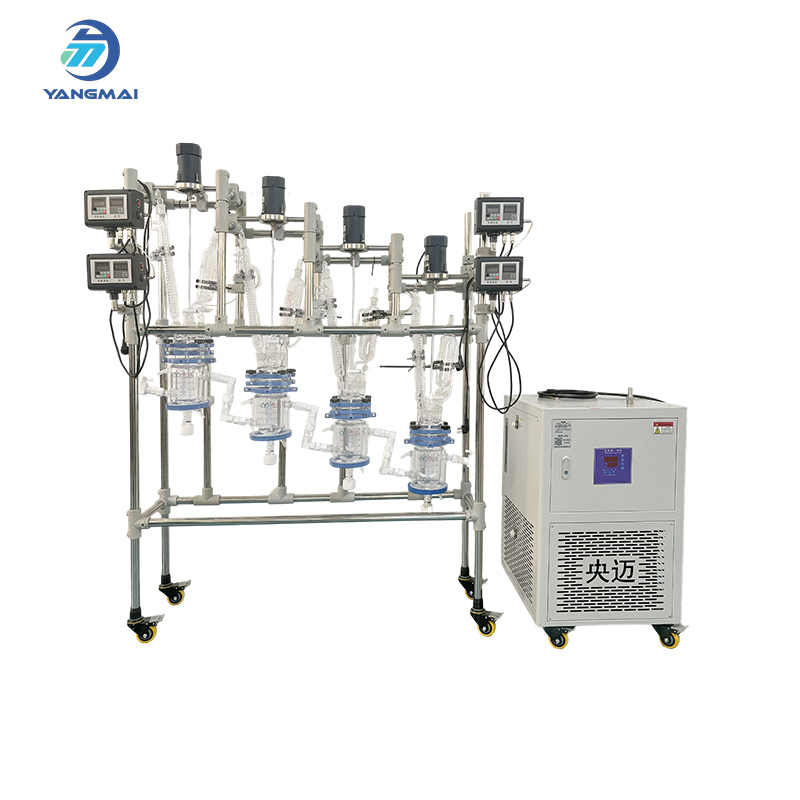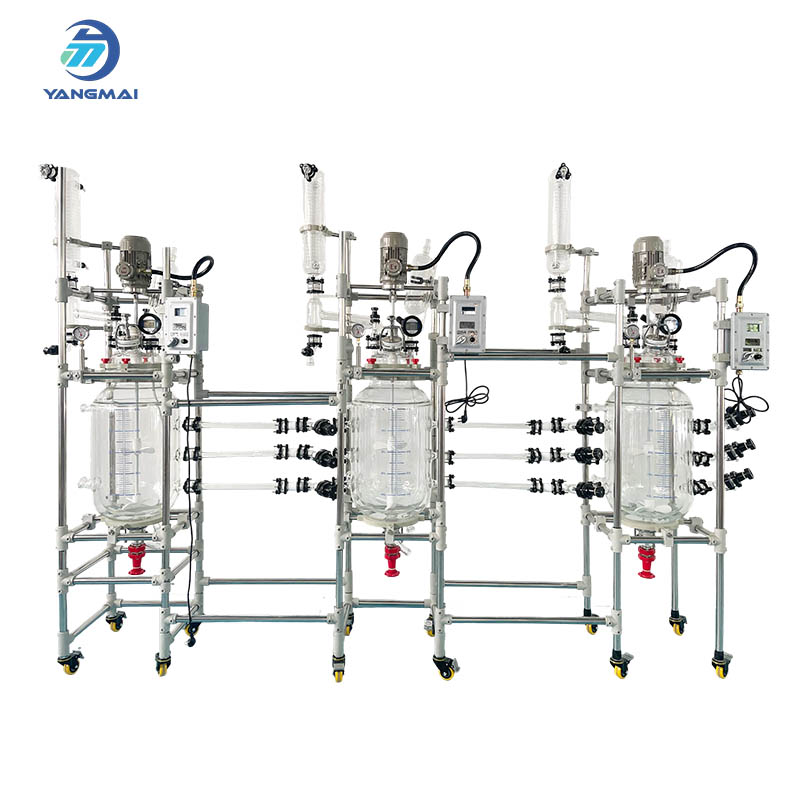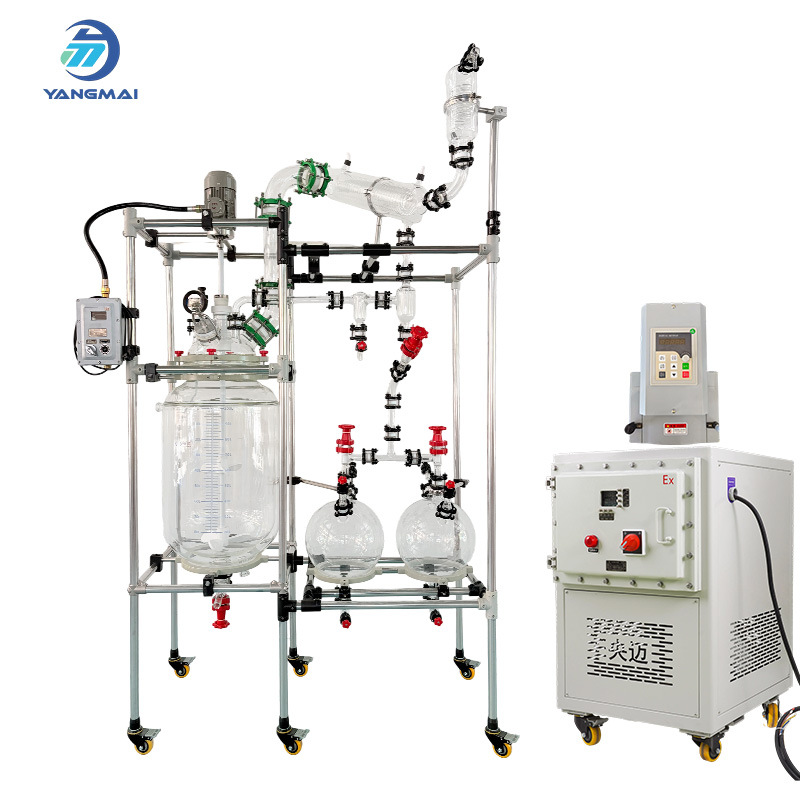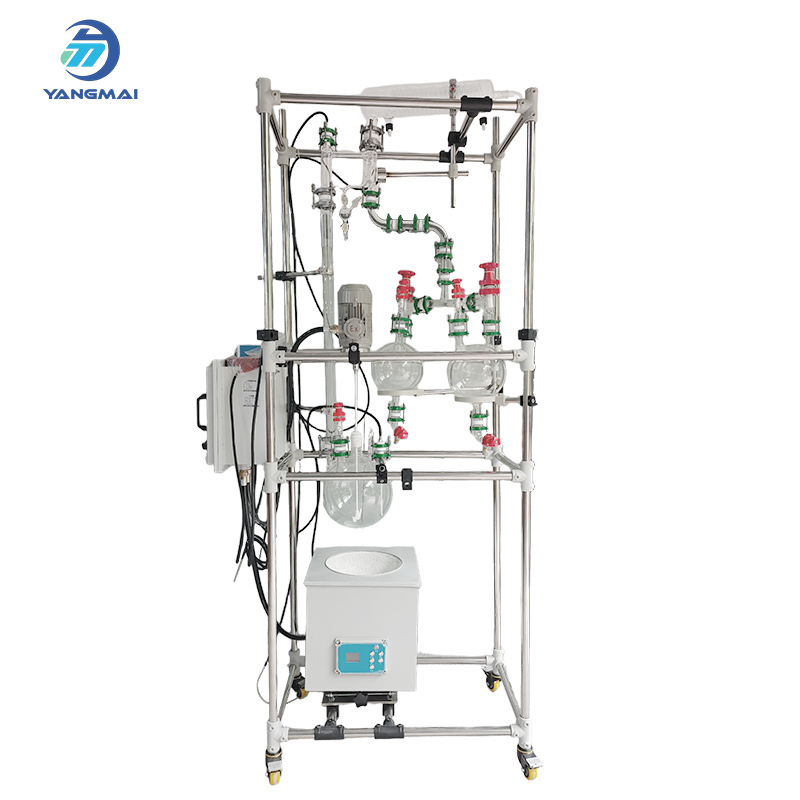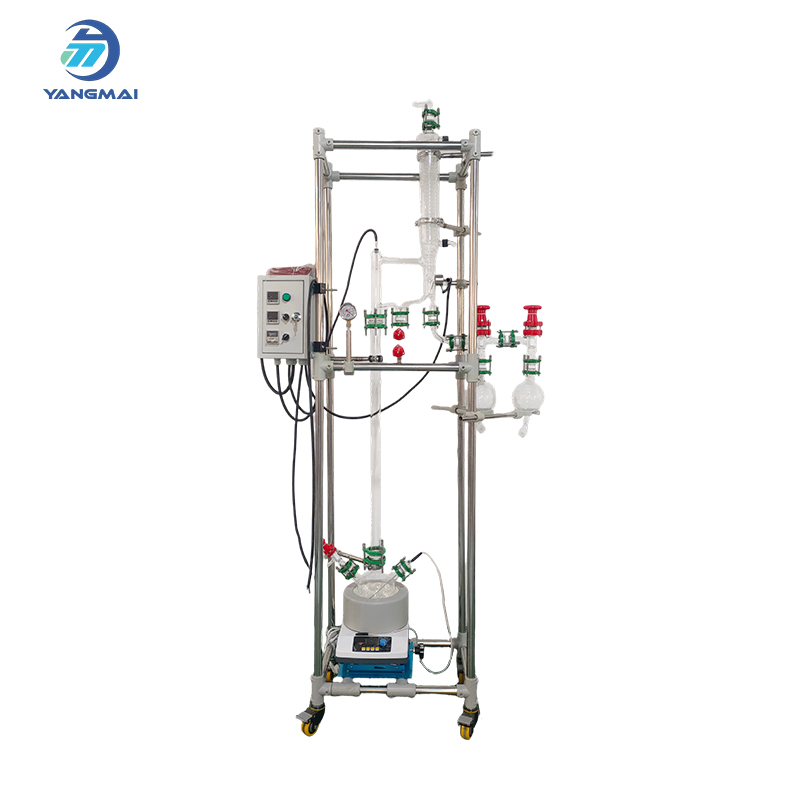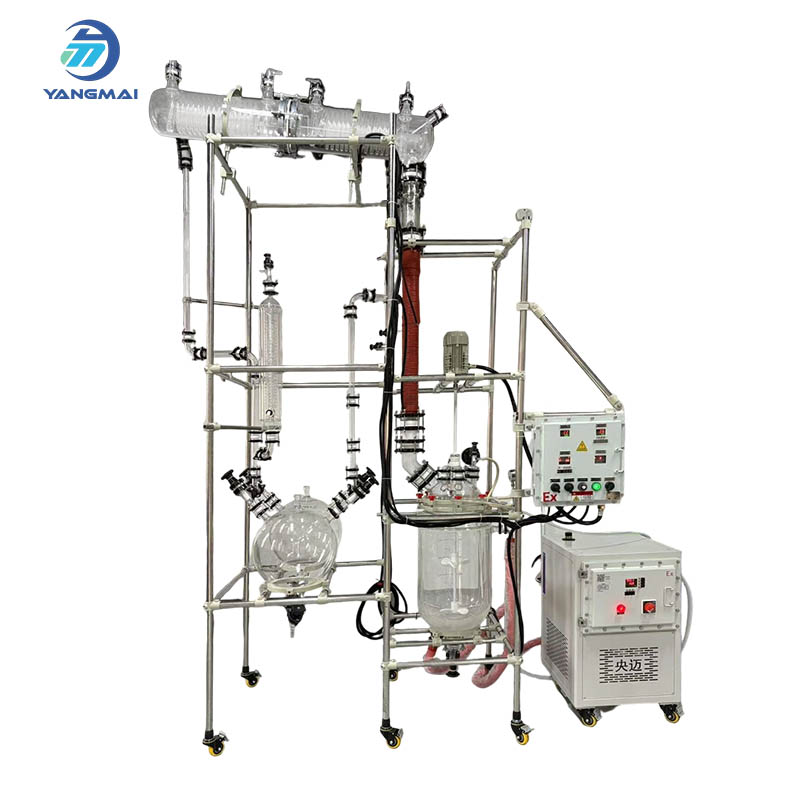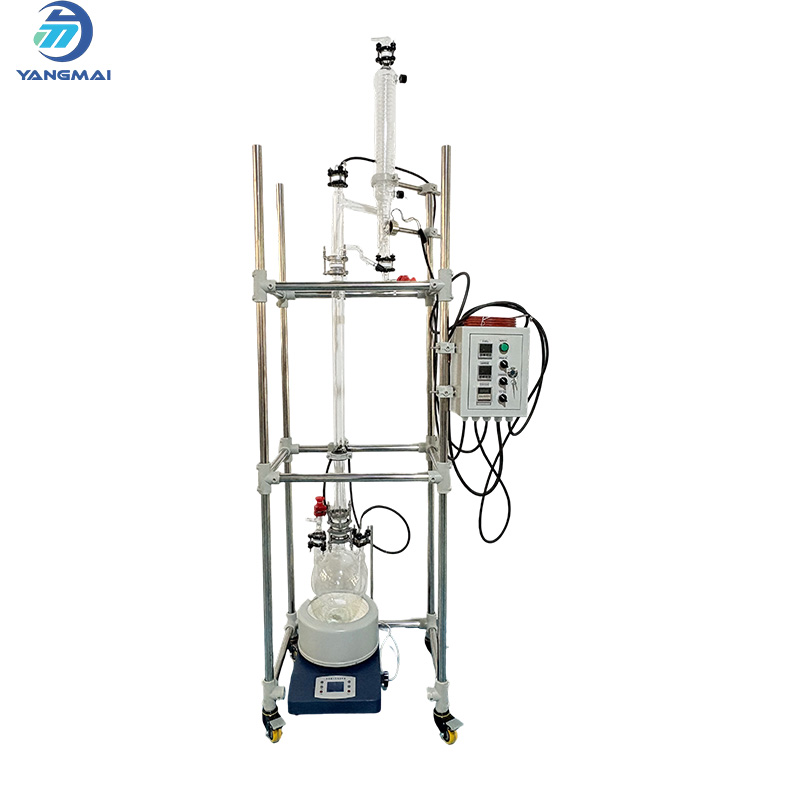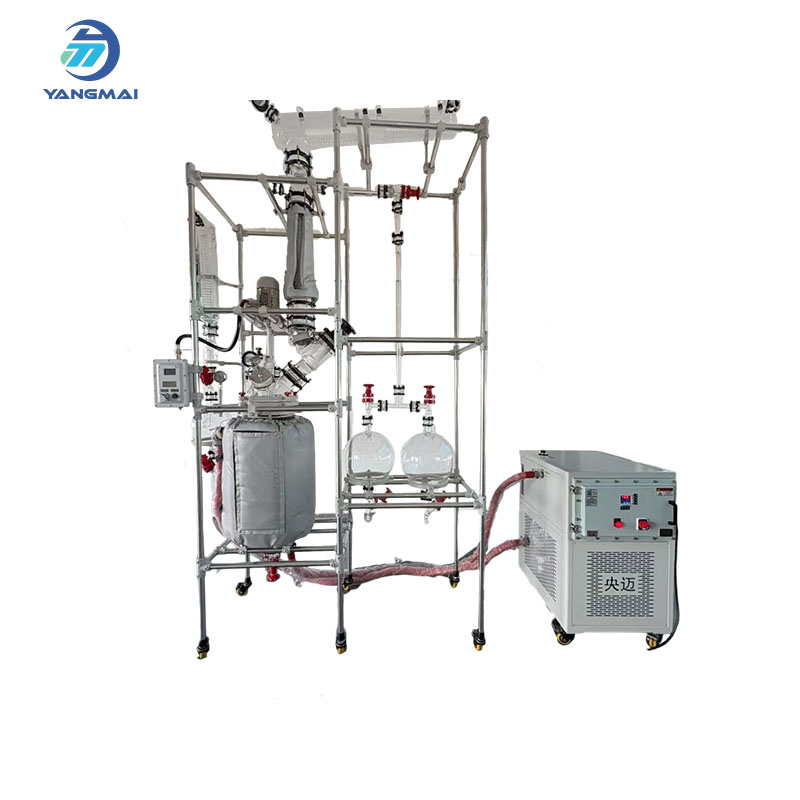
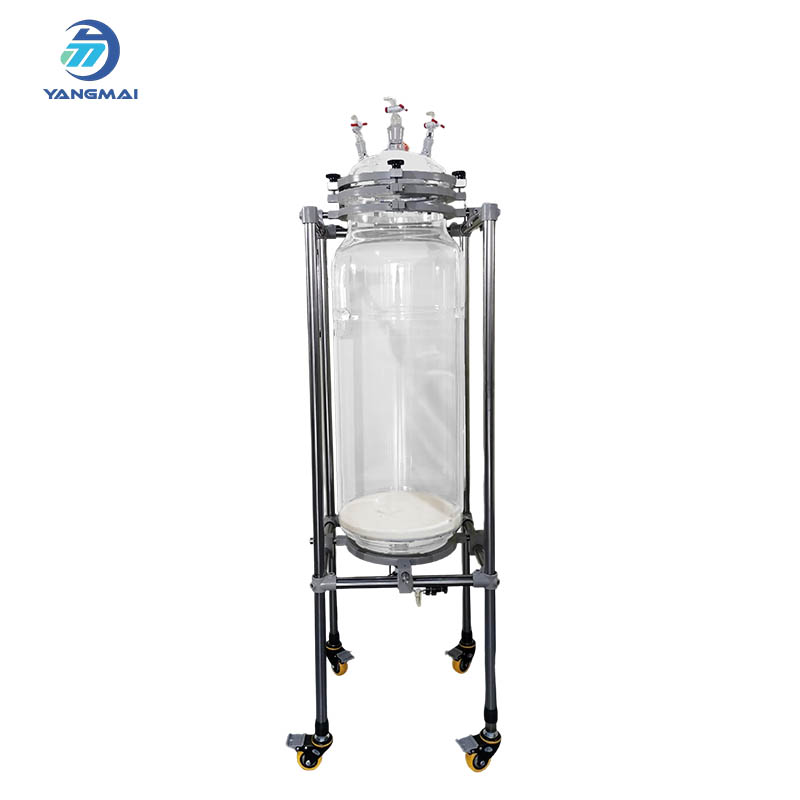
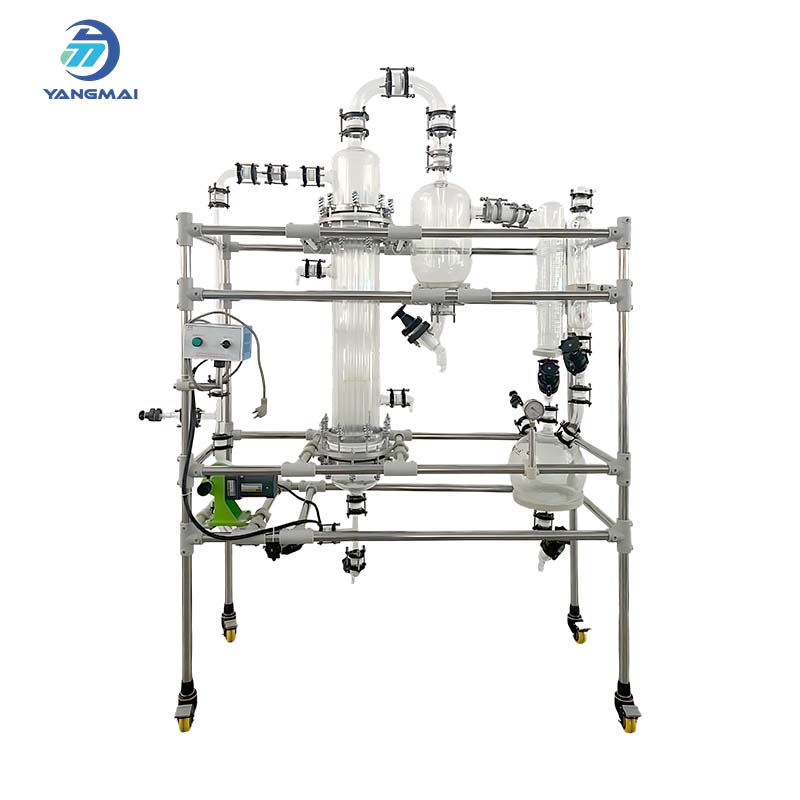
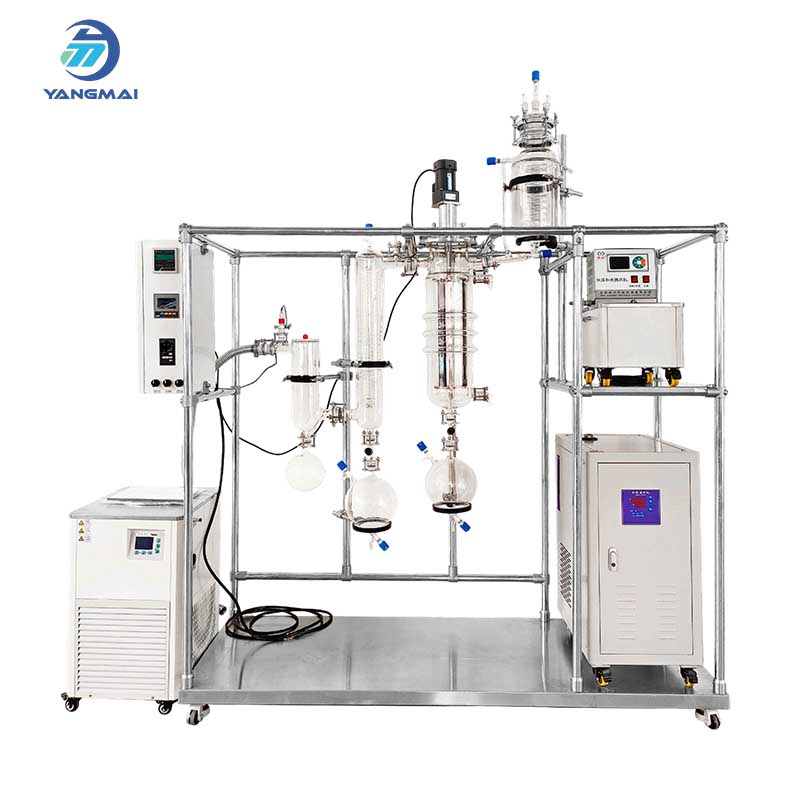
100L jacketed solid phase glass reactor is ideal for handling solid–liquid chemical reactions. It ensures high visibility and precision control for pharmaceutical and lab-scale synthesis.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
High-Capacity Reaction Volume
Reliable Stirring And Mixing System
Accept customized design
50L jacketed solid phase glass reactor is ideal for handling solid–liquid chemical reactions. It ensures high visibility and precision control for pharmaceutical and lab-scale synthesis.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
High-Capacity Reaction Volume
Reliable Stirring And Mixing System
Accept customized design
1L Integrated Glass Reactor is designed for precise laboratory chemical synthesis and provides stable stirring and temperature control performance.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
Continuous Overflow Design
Heavy-Duty Steel Frame
Accept customized design
The Overflow Glass Reactor is designed for precise chemical precipitation and laboratory process research.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
Continuous Overflow Design
Heavy-Duty Steel Frame
Accept customized design
The Overflow Glass Reactor offers safe, stable, and precise reaction control for continuous chemical processes. Built with corrosion-resistant materials, it's ideal for pharmaceutical and organic synthesis labs.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
Continuous Overflow Design
Stable Temperature Control
Heavy-Duty Steel Frame
Accept customized design
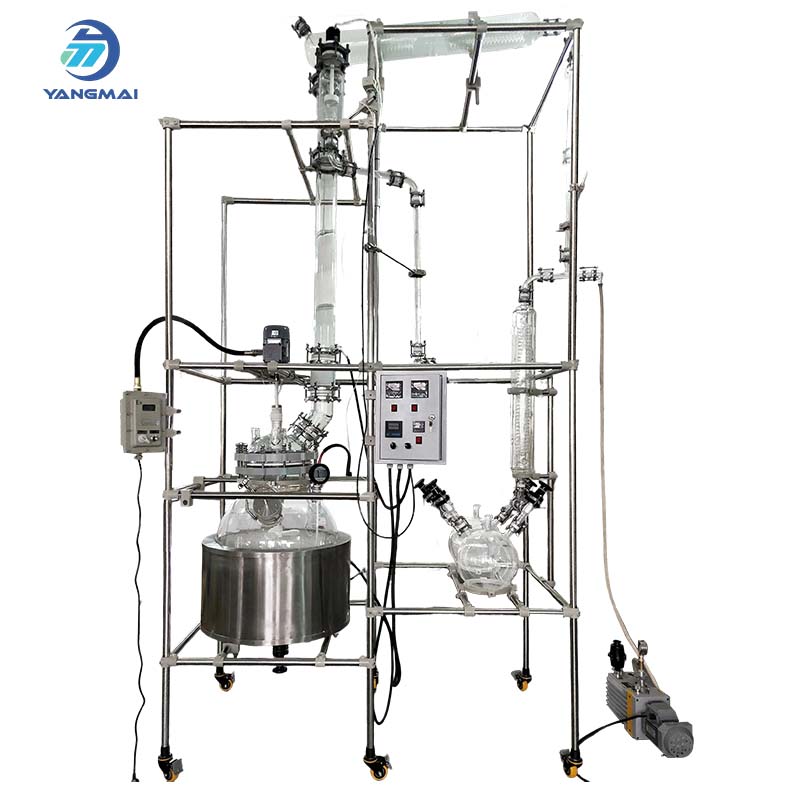
100L Glass Distillation Reactor features a jacketed vessel and built-in condenser, the reactor enables efficient and controlled distillation of complex chemical mixtures.
Excellent Chemical Resistance – Resistant to most acids, alkalis, and organic solvents.
Wide Temperature Range – Operating range: -100°C to +300°C.
Large Reaction Capacity – Suitable for laboratory and pilot-scale applications.
Reliable Stirring System – Ensures stable and uniform mixing.
Customizable Design – Configuration can be tailored to process requirements.
10L Glass Distillation Coulumn is designed for efficient laboratory separation and purification of chemical mixtures.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
High-Capacity Reaction Volume
Reliable Stirring And Mixing System
Accept customized design
2L Glass Distillation Coulumn is designed for solvent purification, rectification, and recovery during chemical synthesis experiments. Its vertical structure allows efficient vapor–liquid contact for improved separation performance.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
High-Capacity Reaction Volume
Reliable Stirring And Mixing System
Accept customized design
50L Glass Distillation Reactor is designed with a jacketed body and integrated condenser, this reactor ensures efficient distillation of complex chemical mixtures under controlled conditions.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
High-Capacity Reaction Volume
Reliable Stirring And Mixing System
Accept customized design
5L Glass Distillation Reactor is designed for fractional separation, solvent recovery, and chemical process research.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
High-Capacity Reaction Volume
Reliable Stirring And Mixing System
Accept customized design
100L Glass Distillation Reactor is designed for fractional separation, solvent recovery, and chemical process research.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
High-Capacity Reaction Volume
Reliable Stirring And Mixing System
Accept customized design
100L Glass Distillation Reactor is designed with a jacketed body and integrated condenser, this reactor ensures efficient distillation of complex chemical mixtures under controlled conditions.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
High-Capacity Reaction Volume
Reliable Stirring And Mixing System
Accept customized design