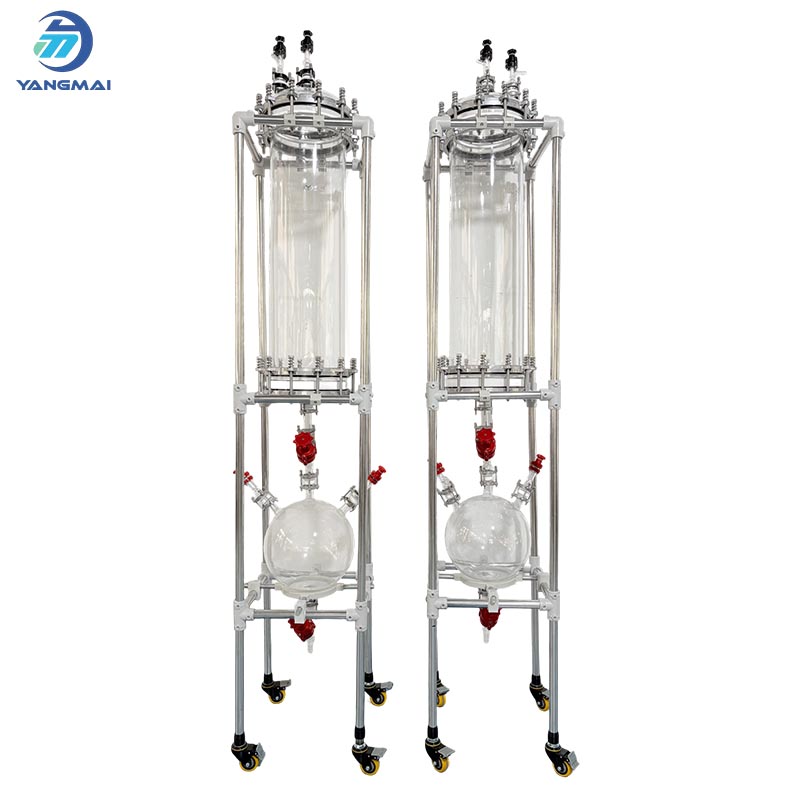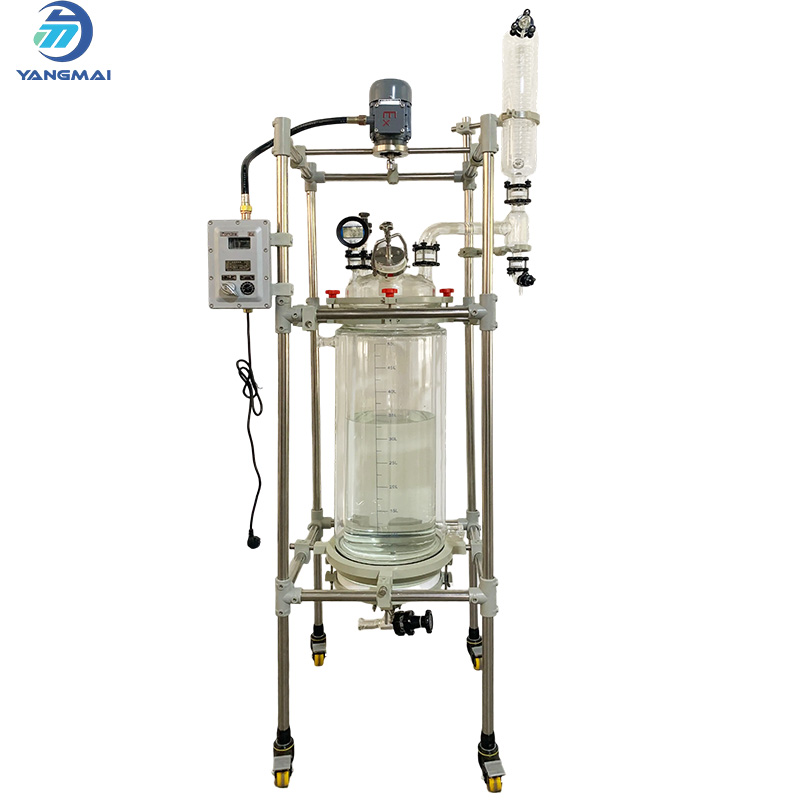
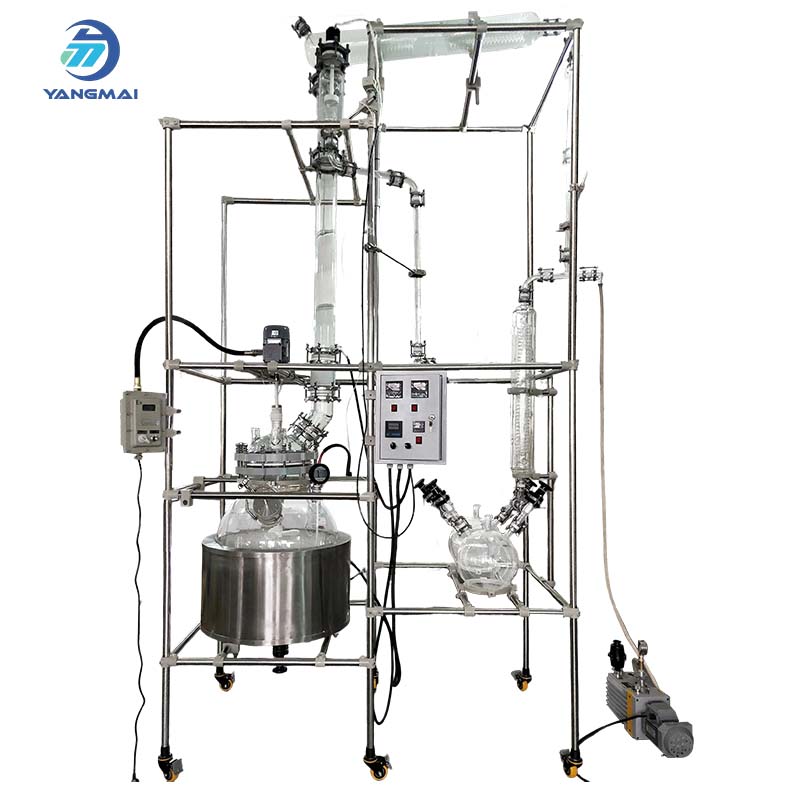
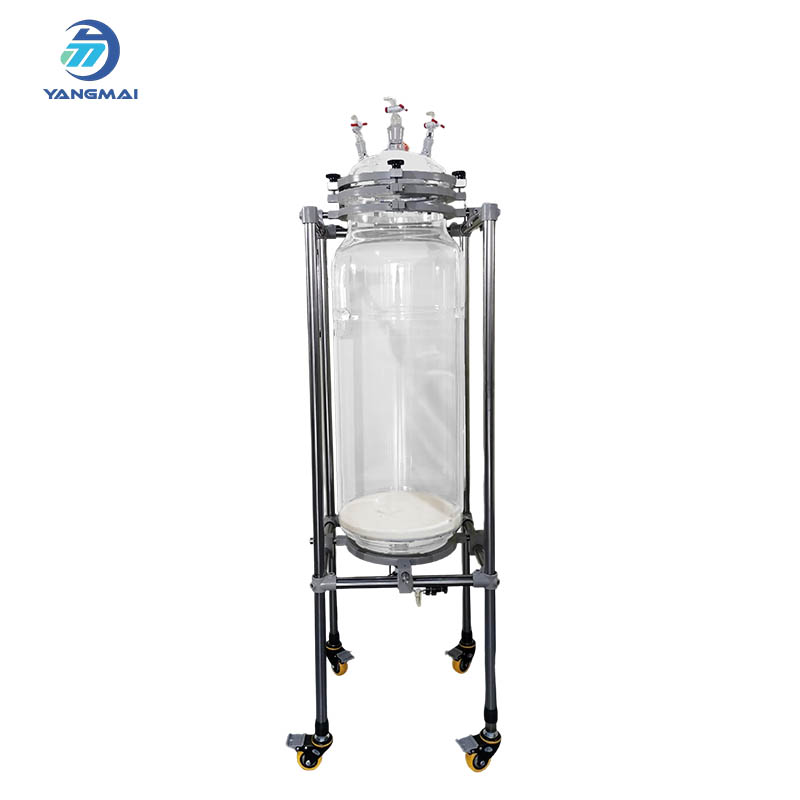
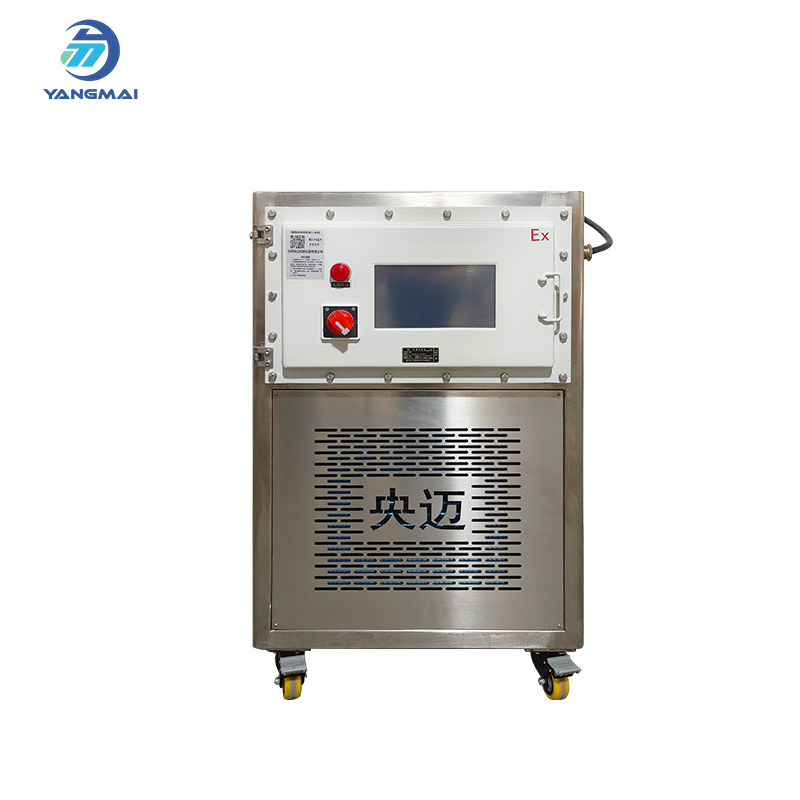
70L Glass Filtration Reactor is a versatile lab system for efficient solid-liquid separation and crystallization. It features a glass reactor for precise temperature control and a bottom filtration unit for seamless material separation. Mounted on a mobile, sturdy frame, it is ideal for laboratory and pilot-scale applications.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -105℃~300℃
Visible Filtration Process
Corrosion-Proof Filtration System
Accept Customized Design
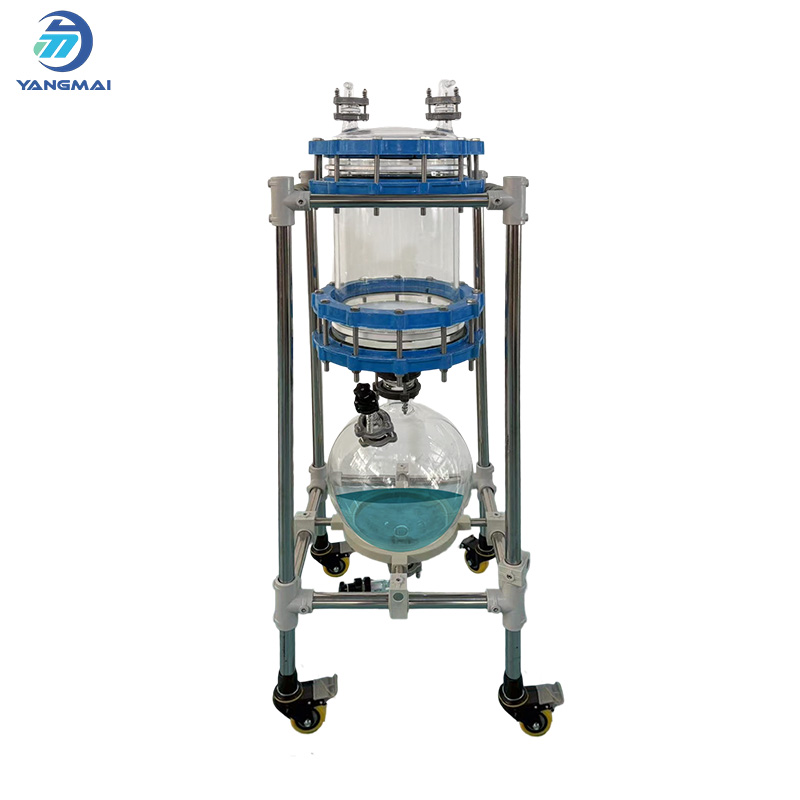
20L Glass Filtration Reactor is a versatile lab system for efficient solid-liquid separation and crystallization. It features a glass reactor for precise temperature control and a bottom filtration unit for seamless material separation. Mounted on a mobile, sturdy frame, it is ideal for laboratory and pilot-scale applications.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -105℃~300℃
Visible Filtration Process
Corrosion-Proof Filtration System
Accept Customized Design
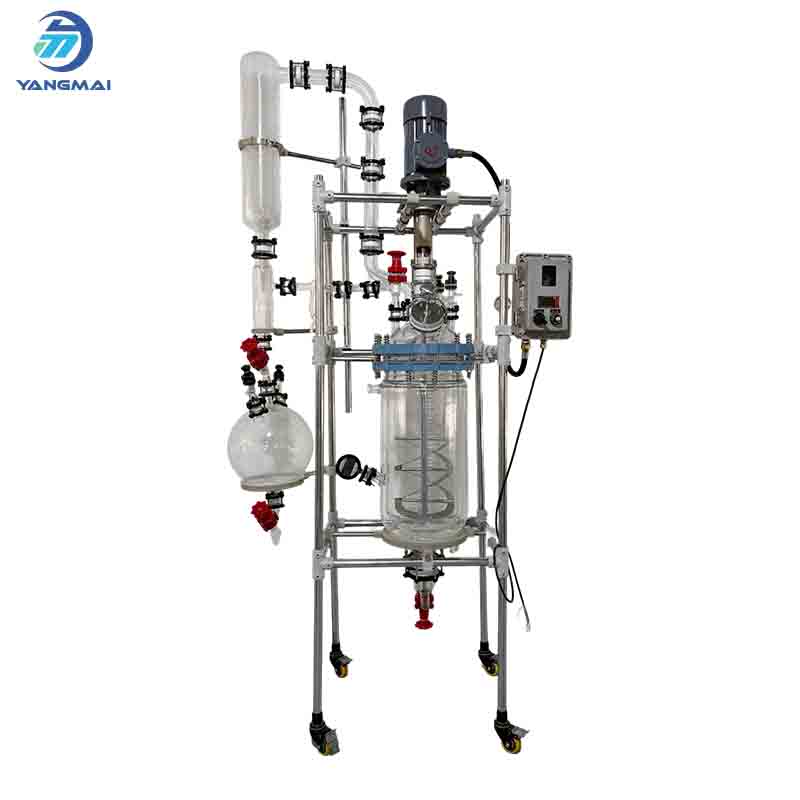
40L Jacketed Glass Reactor is a versatile piece of equipment widely used in chemical, pharmaceutical, food, and biotech industries.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -105℃~300℃
Transparent and easy to observe
Accept customized design
50L Jacketed Glass Filter Reactor is a versatile piece of equipment widely used in chemical, pharmaceutical, food, and biotech industries.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -105℃~300℃
Transparent and easy to observe
Accept customized design
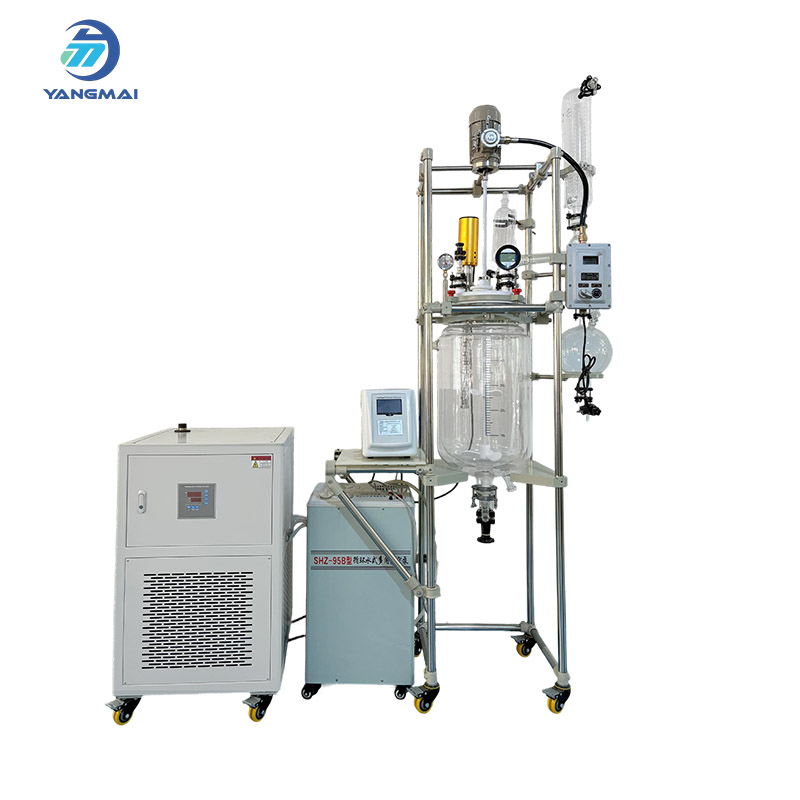
50L glass reactor comes integrated with an ultrasonic probe for efficient chemical extraction and dispersion. Ideal for pharmaceutical R&D, organic synthesis, and cell disruption experiments.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
Transparent and easy to observe
Accept customized design
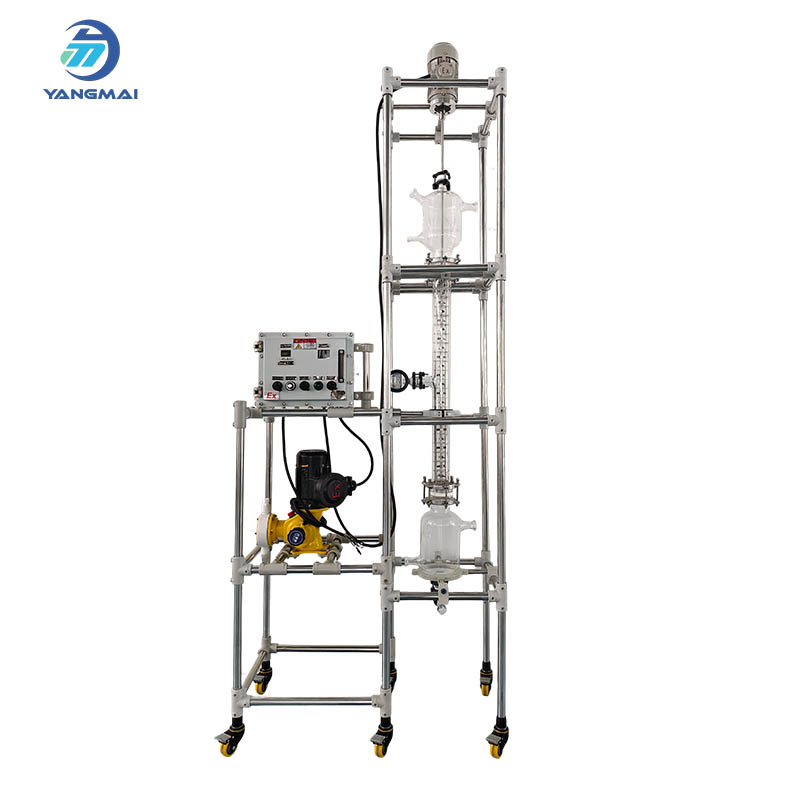
Advanced rotating disc contactor ideal for high-efficiency liquid-liquid extraction in chemical and pharmaceutical industries.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
Transparent and easy to observe
Accept customized design
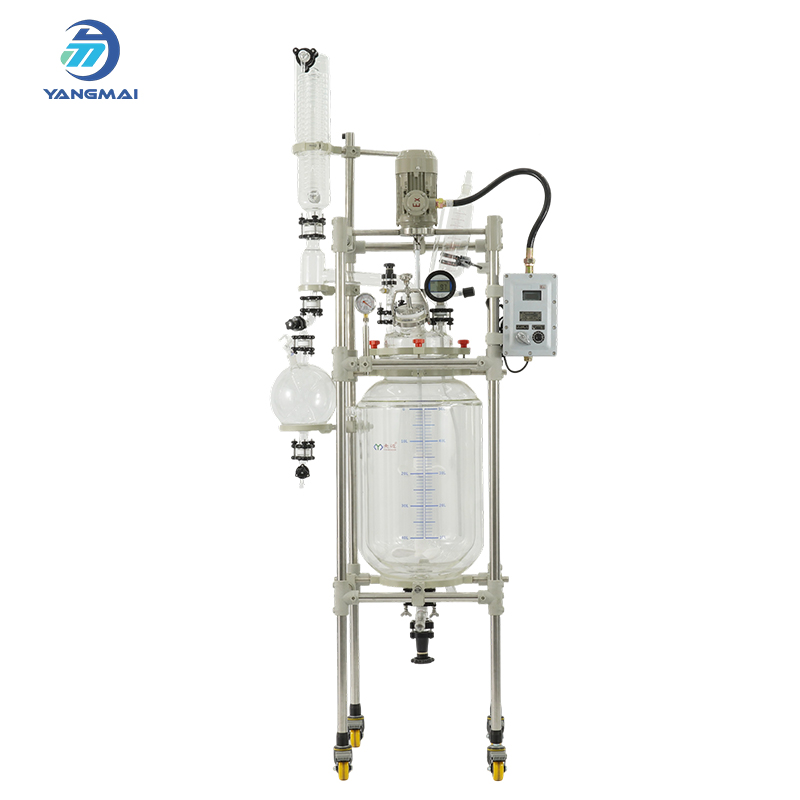
50 L jacketed glass reactor is a versatile piece of equipment widely used in chemical, pharmaceutical, food, and biotech industries.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
Transparent and easy to observe
Accept customized design
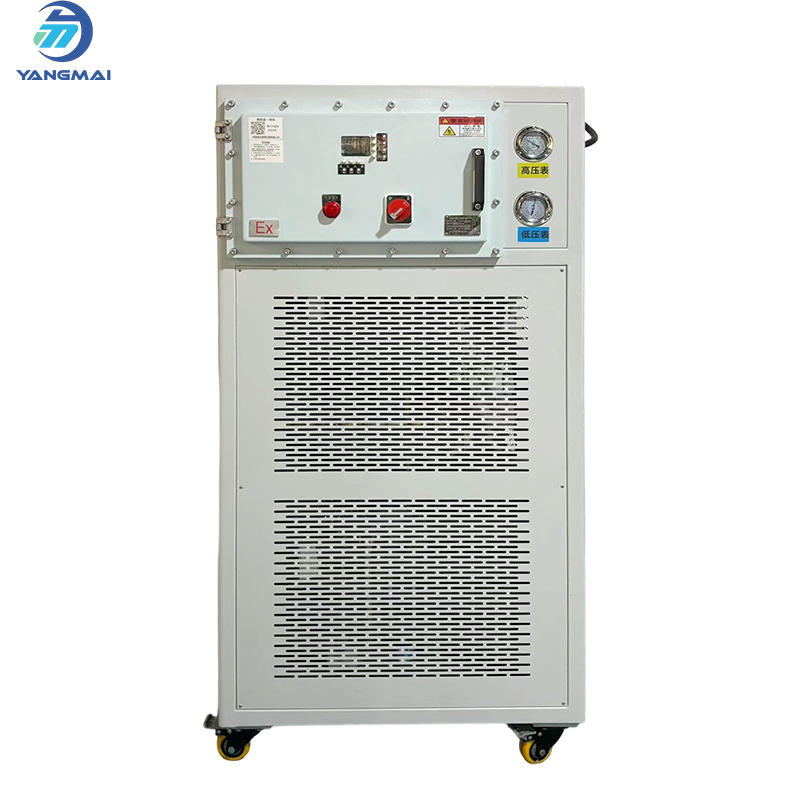
The 300L explosion-proof high-low temperature circulator integrates heating and cooling in one unit for precise thermal control. Ideal for supporting glass reactors in chemical laboratories with enhanced safety and stability.
Feature:
Wide temperature range: -30℃~300℃
Explosion-Proof Design: Ensures safe operation in flammable environments.
Dual Temperature Function: Integrated heating and cooling in one system.
Eco-Friendly Refrigerants: Reduces environmental impact.
Accept customized design
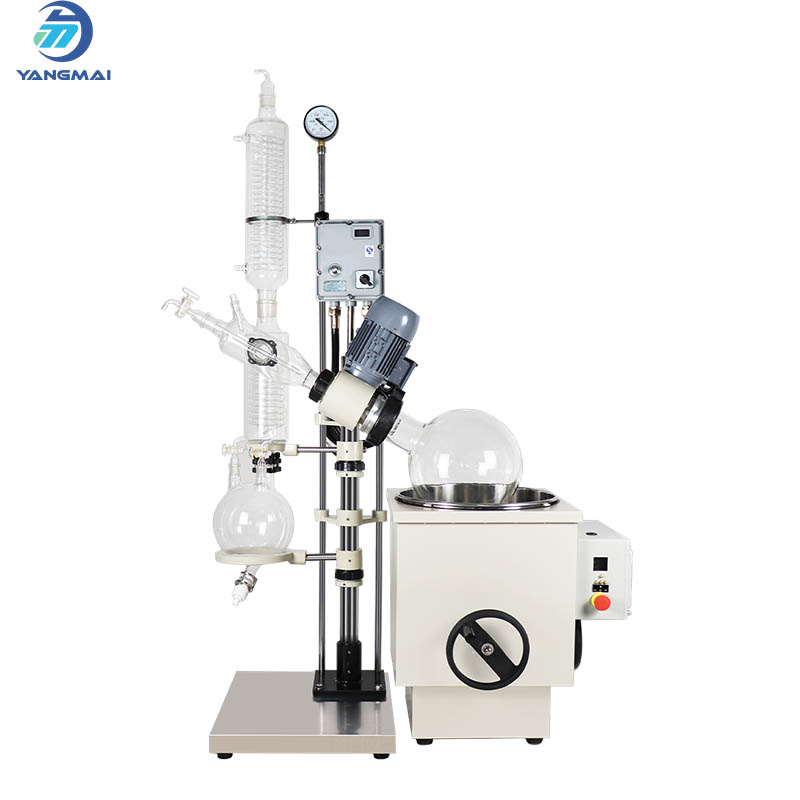
The 10L Glass Rotary Evaporator ensures fast solvent removal with stable performance. It is ideal for laboratory extraction and chemical purification.
Feature:
High Evaporation Efficiency
Durable Borosilicate Glass Body
Oil/Water Bath Dual Usage
Corrosion-Resistant Components
Accept Customized Design
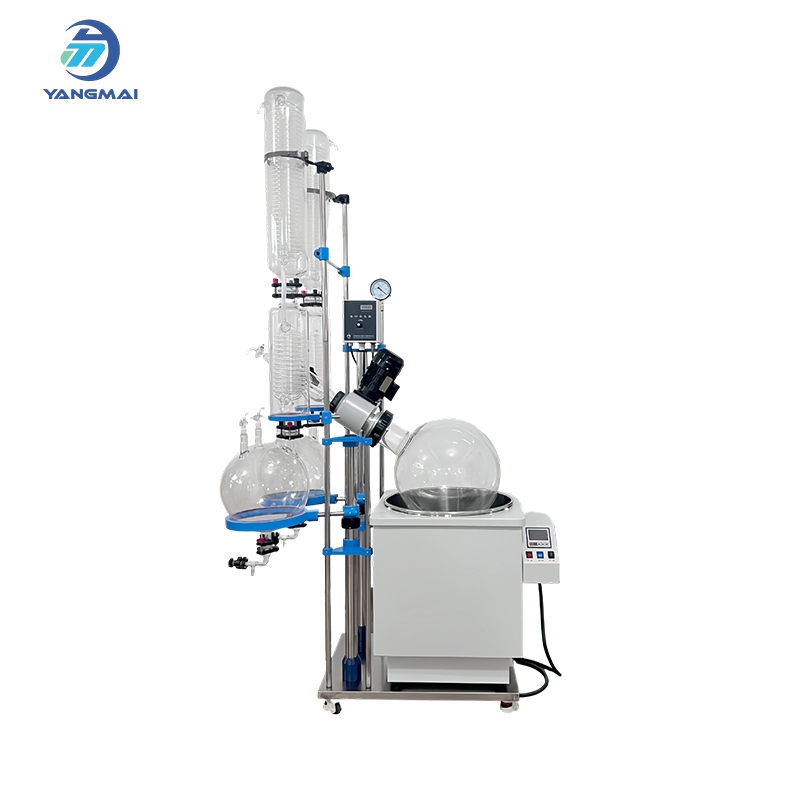
The 50L Rotary Evaporator is a high-performance vacuum evaporation and concentration system designed for efficient solvent recovery, separation, and purification in laboratories, pharmaceutical research, chemical processing, and pilot-scale applications.
Featuring a 50L rotating evaporation flask, an efficient condensation system, and adjustable rotation speed, this rotary evaporator enables gentle and uniform evaporation under reduced pressure. Vacuum operation lowers the boiling point of solvents, making it particularly suitable for heat-sensitive materials.
Constructed with high-quality borosilicate glass and corrosion-resistant PTFE components, the system offers excellent chemical compatibility, clear process visibility, and reliable operation.
Key Features:
50L Large Capacity: Ideal for laboratory and pilot-scale evaporation applications.
Efficient Vacuum Evaporation: Reduces solvent boiling temperatures for gentle concentration.
High-Efficiency Condensation: Supports effective solvent recovery and collection.
Adjustable Rotation Speed: Promotes uniform heating and improves evaporation efficiency.
Borosilicate Glass Construction: Provides excellent chemical resistance and clear process observation.
Wide Applications: Suitable for solvent recovery, herbal extraction, pharmaceutical research, and chemical concentration.
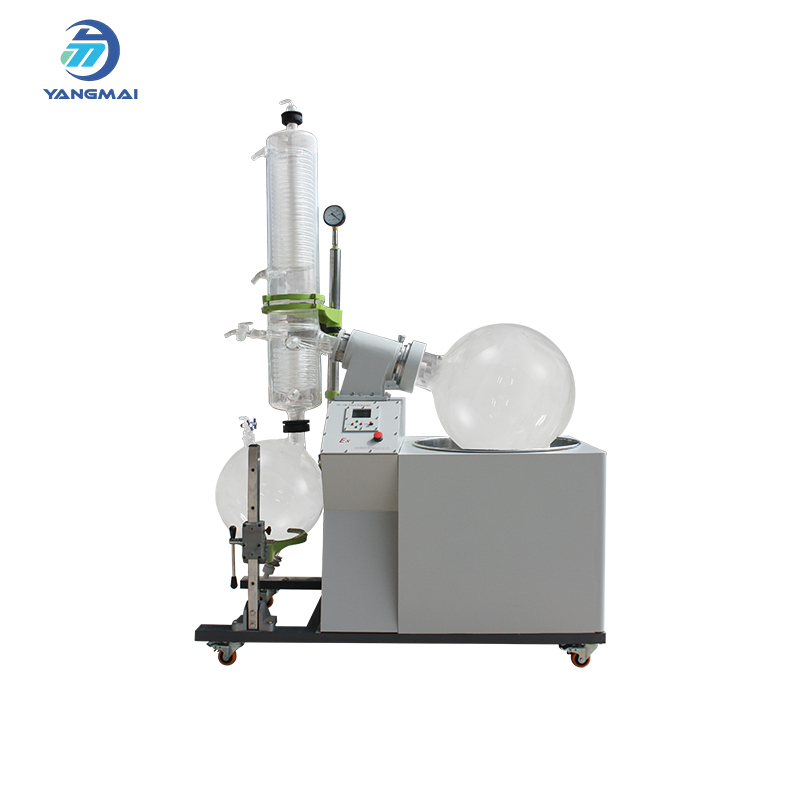
The 100L rotary evaporator ensures efficient solvent recovery with precise temperature control, ideal for laboratory-scale extractions. It features a durable design and easy operation.
Feature:
High Evaporation Efficiency
Durable Borosilicate Glass Body
Oil/Water Bath Dual Usage
Corrosion-Resistant Components
Accept Customized Design
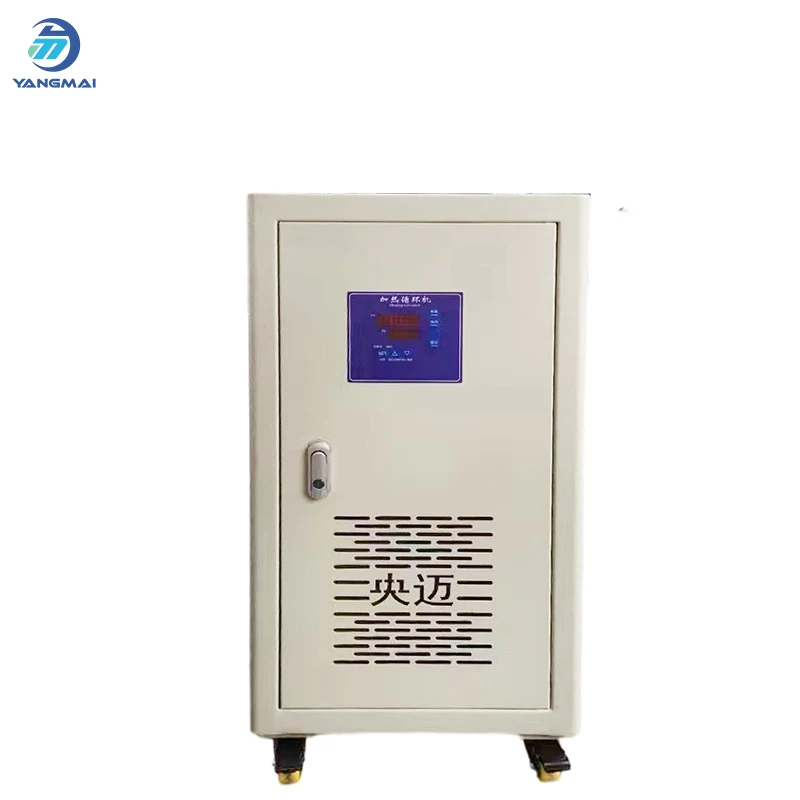
The 20L Heating Recirculating Machine provides stable and efficient temperature control for laboratory and pilot-scale chemical processes. It is designed for continuous operation with reliable thermal performance and precise regulation.
Feature:
Wide Temperature Range
Precise PID Control
Durable Housing
Continuous Temperature Regulation
Customizable Design