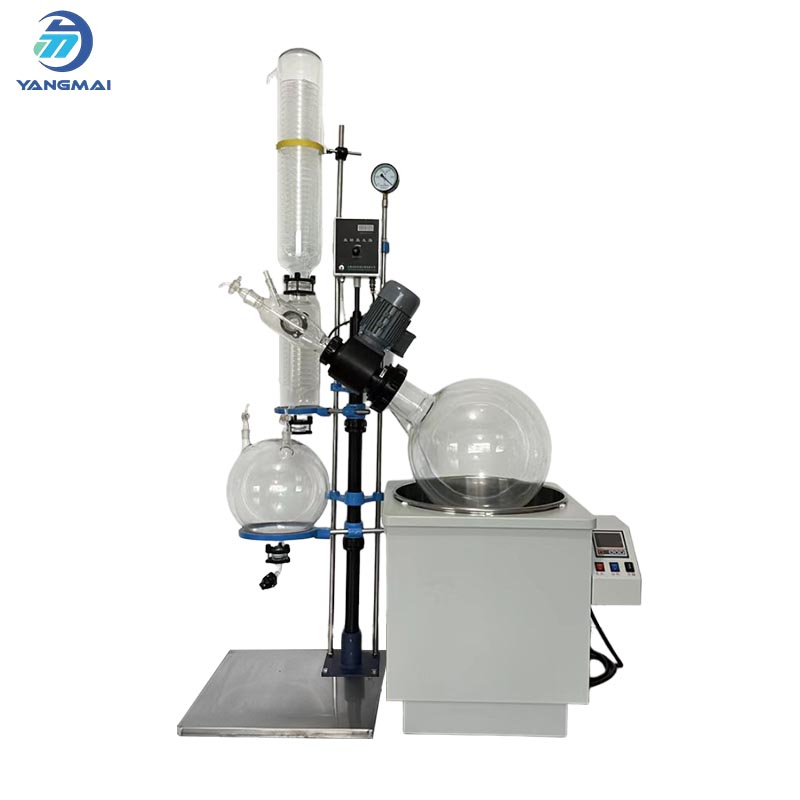
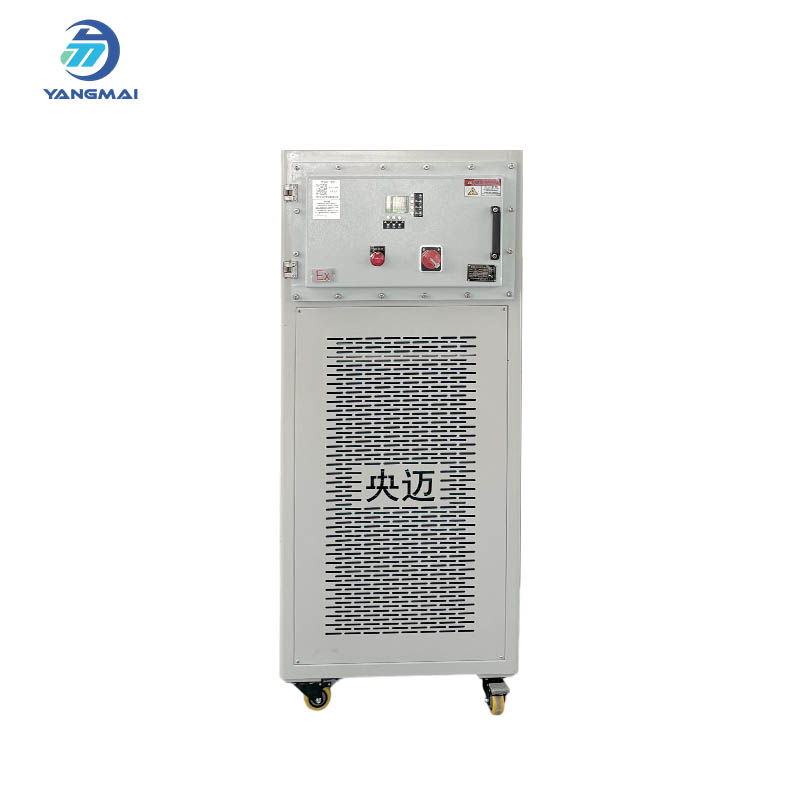
The 20L Rotary Evaporator is designed for efficient solvent evaporation and recovery with stable temperature control, making it suitable for laboratory-scale extraction and concentration processes. Its robust construction and user-friendly operation provide reliable performance for routine laboratory applications.
Feature:
High Evaporation Efficiency
Precise Temperature Control
Adjustable Rotation Speed
Corrosion-Resistant Glass
Reliable Vacuum Sealing
Easy Manual Lifting
Oil/Water Bath Compatible
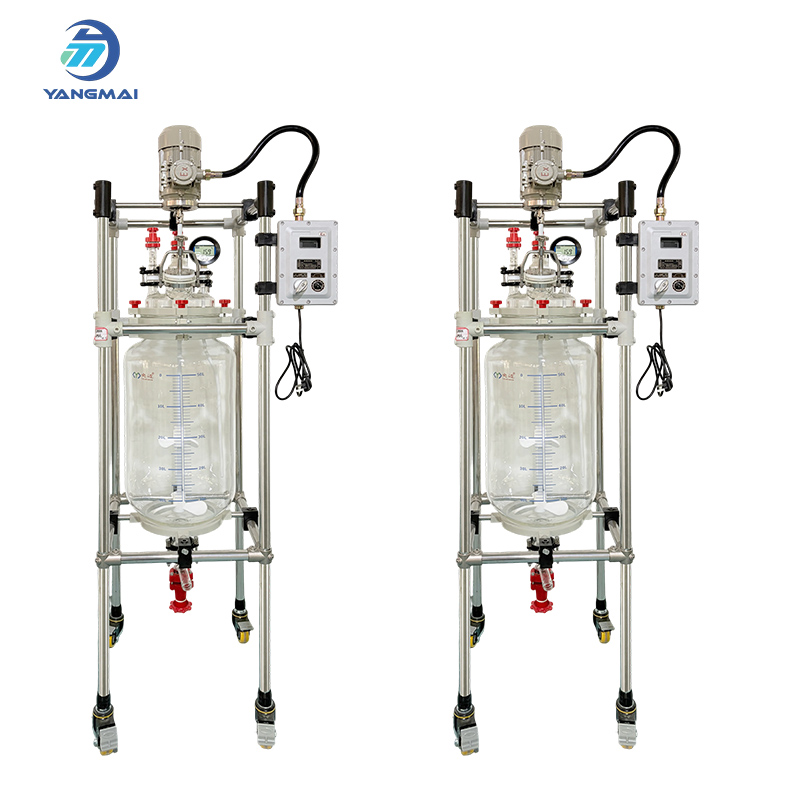
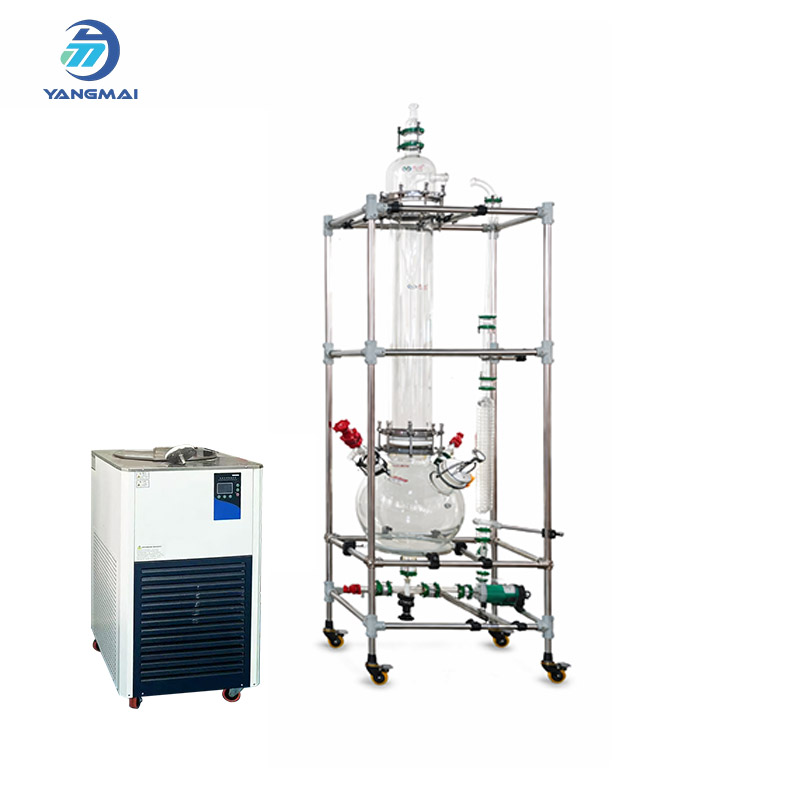
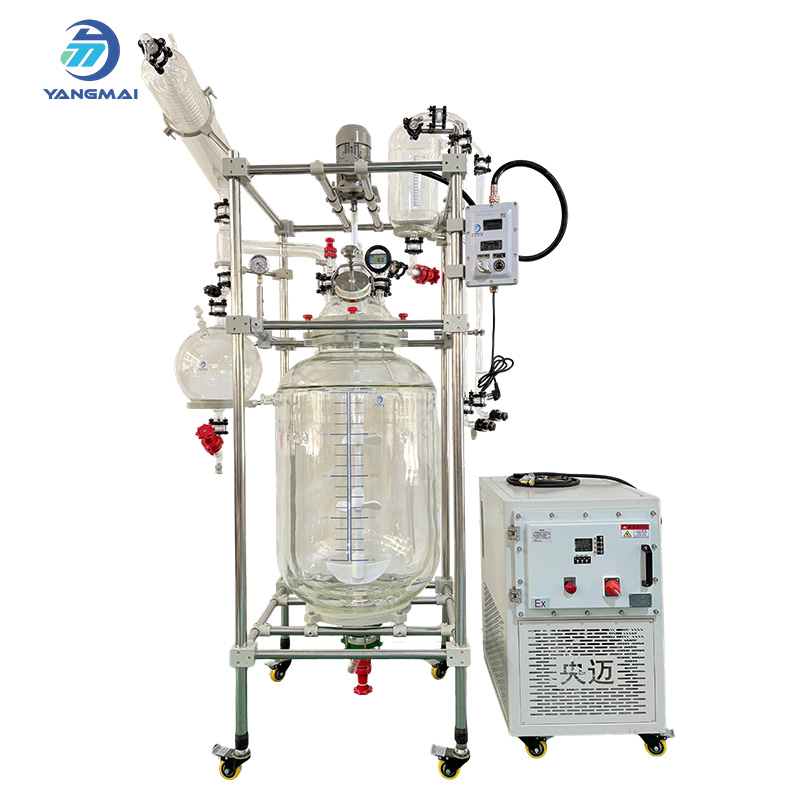
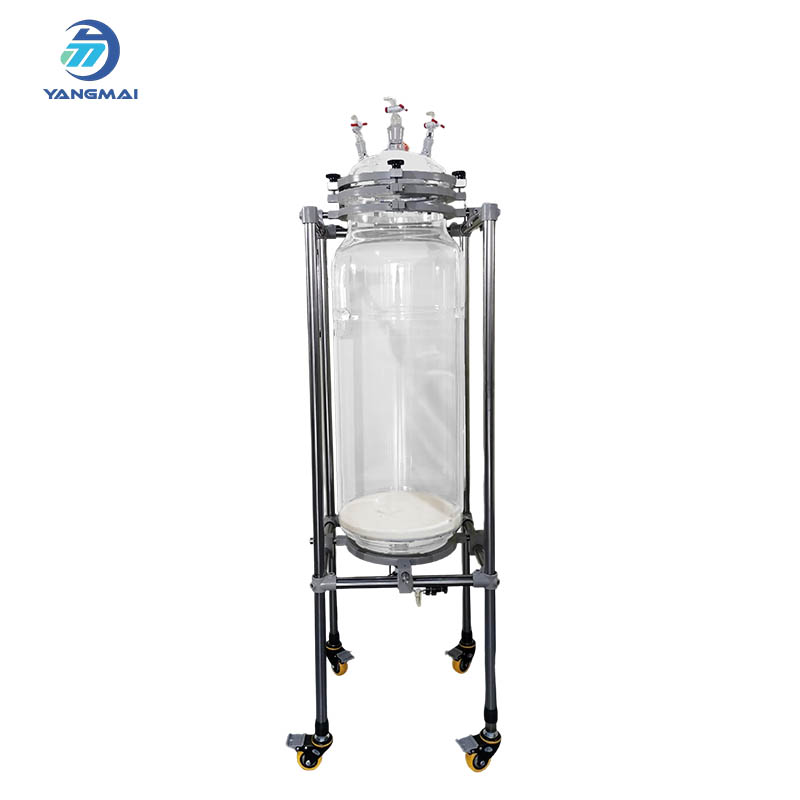
The 50L single-layer glass reactor is designed for mixing, synthesis, and solvent processing under atmospheric or vacuum conditions. Its transparent structure supports accurate laboratory observation and reaction control.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
Explosion-Proof Motor
Solvent Resistant Borosilicate Glass
Heavy-Duty Steel Frame
Accept customized design
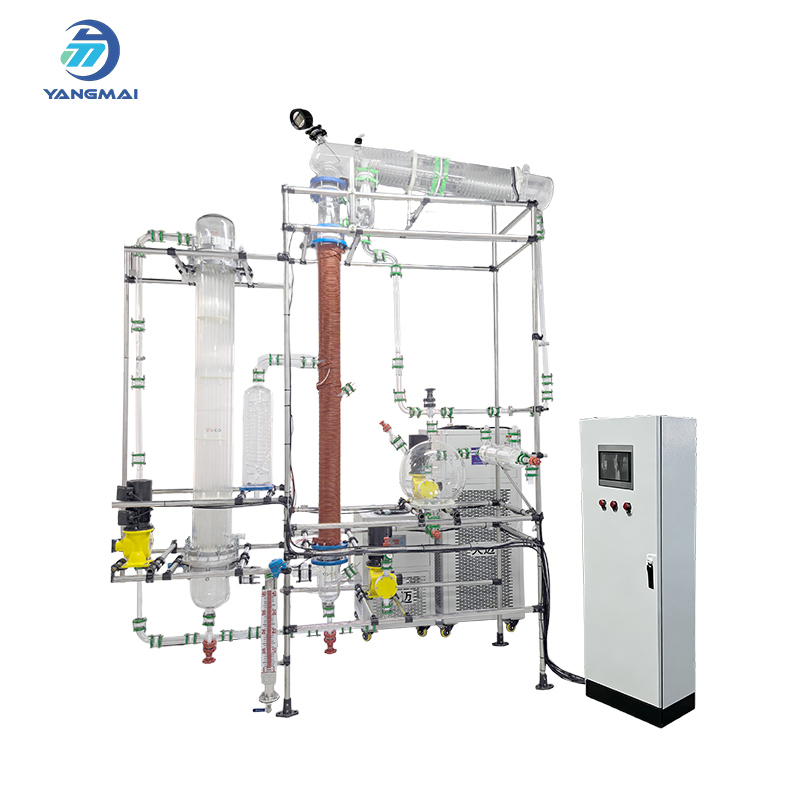
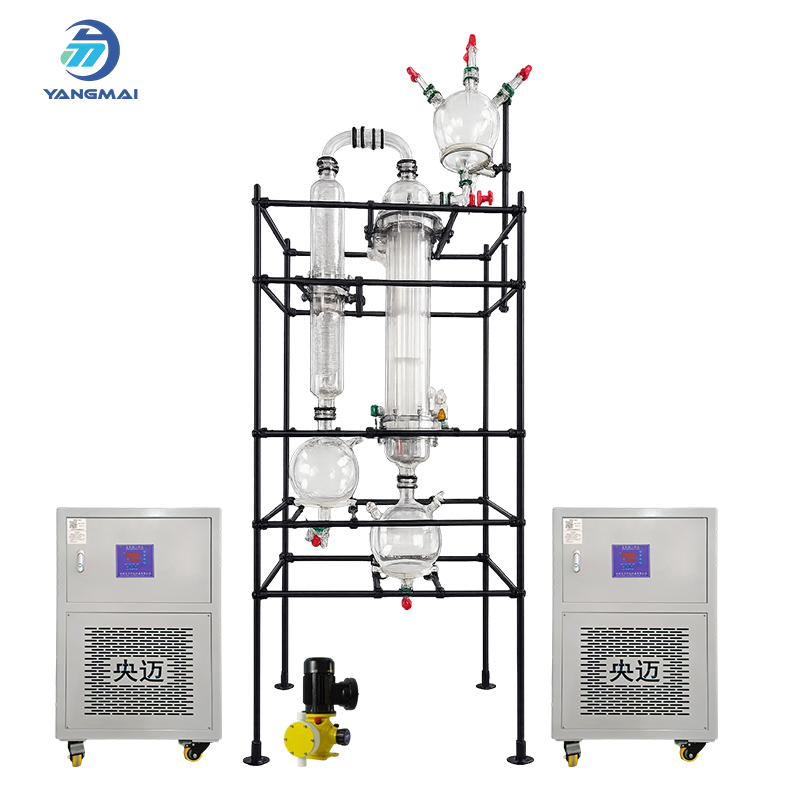
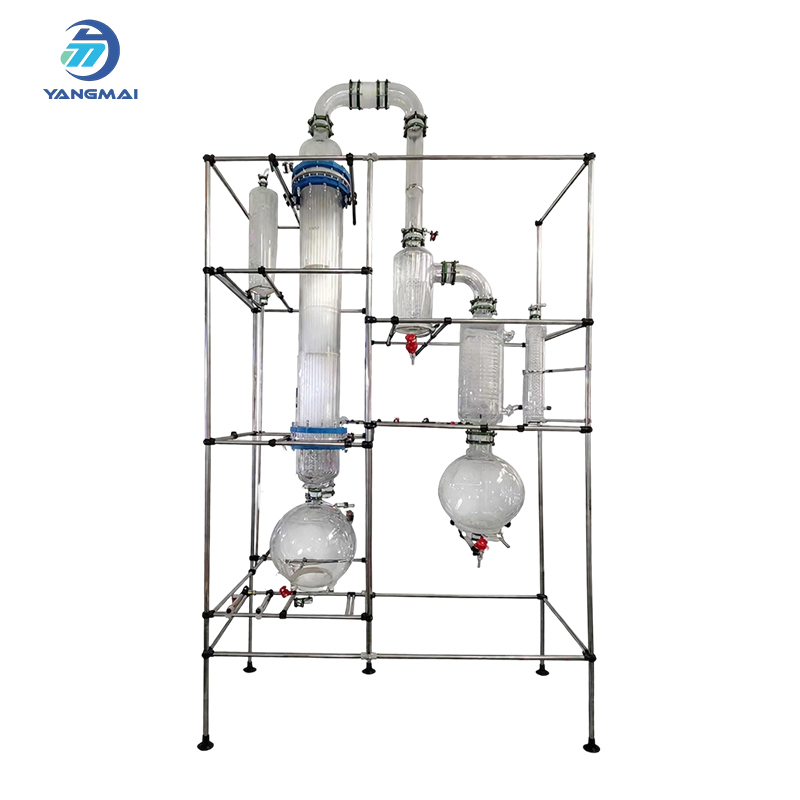
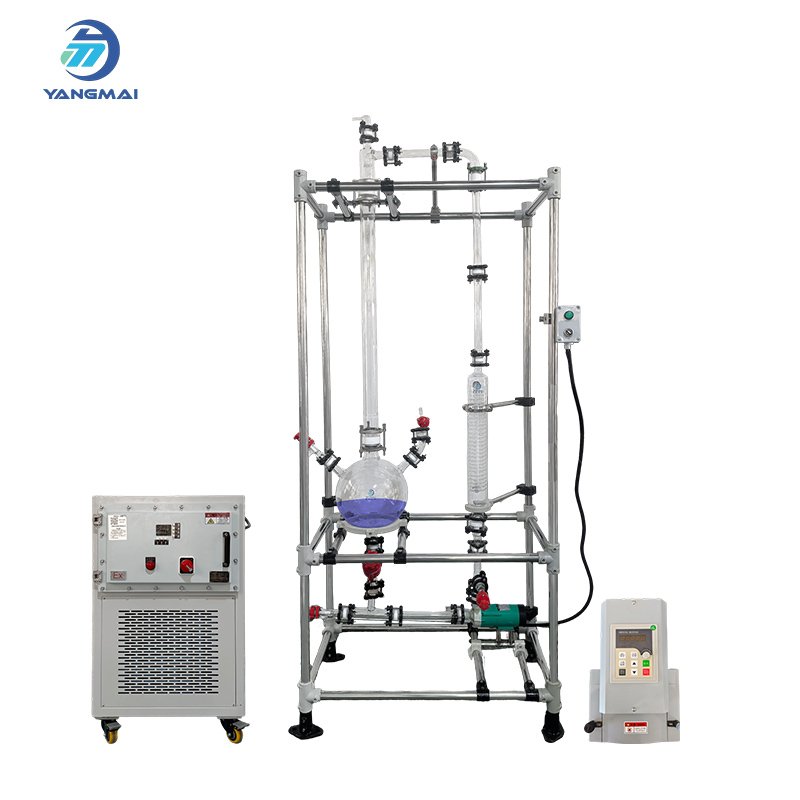
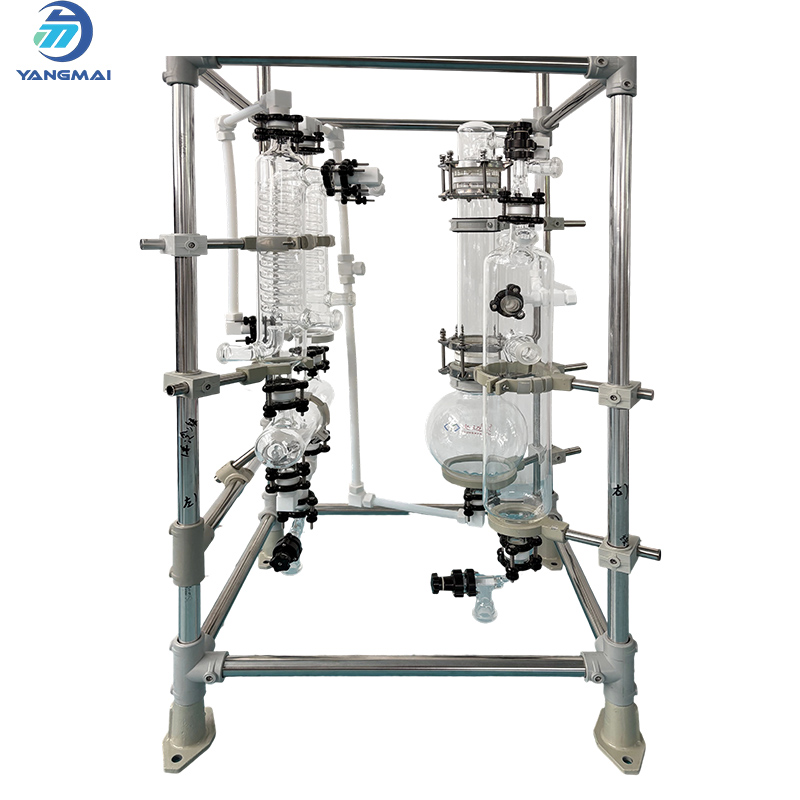
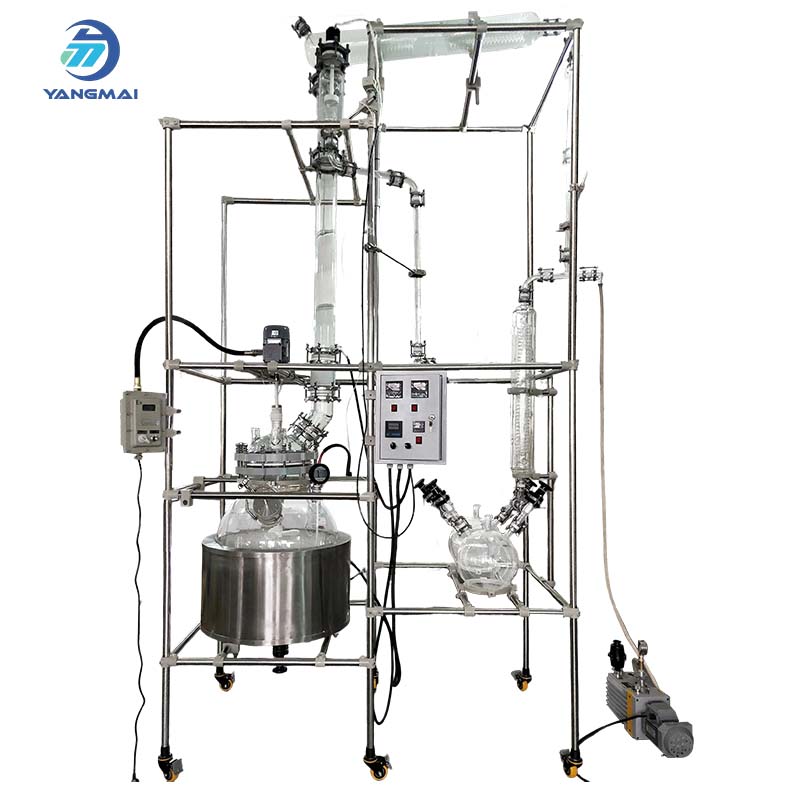
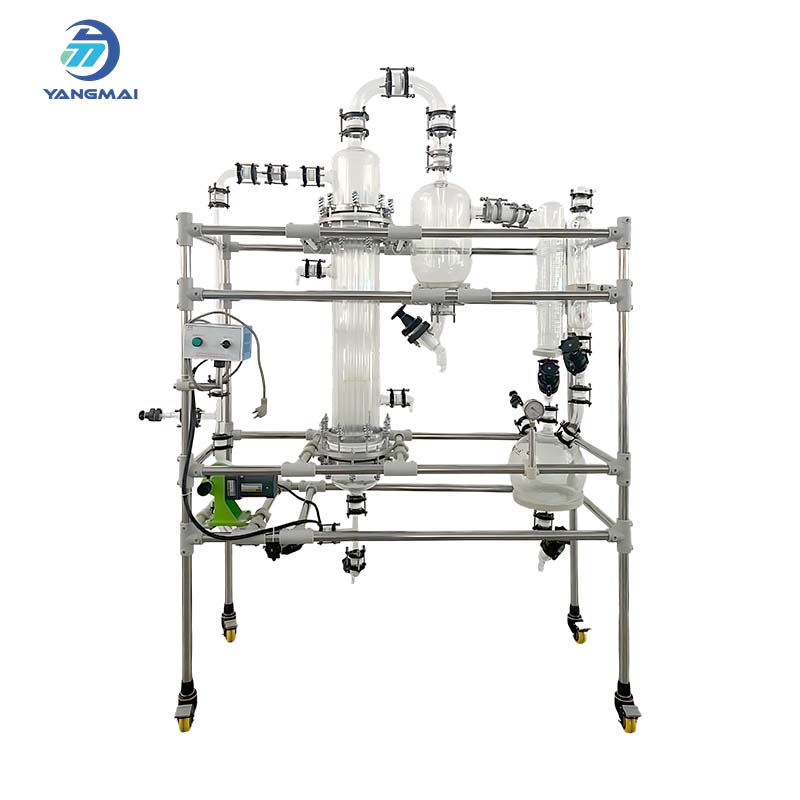
The Glass Falling Film Distillation System is designed for efficient solvent evaporation and fractional purification under vacuum conditions. It is suitable for heat-sensitive materials and continuous laboratory processing.
Feature:
High-Efficiency Falling Film Technology
Short Solution Residence Time
High Heat Transfer And Evaporation Efficiency
Transparency And Clarity
Corrosion Resistance
The 3m² Glass Falling Film Evaporator is ideal for visible and controllable chemical reactions at lab or pilot scale. Perfect for extraction, alkylation, and organic compound synthesis.
Feature:
Large Unit Heating Area
Short Solution Residence Time
High Heat Transfer And Evaporation Efficiency
Transparency And Clarity
Corrosion Resistance
The glass coil condenser provides efficient, corrosion-resistant heat transfer for high-purity applications such as solvent condensation and acid recovery.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Max operation temperature range: 200℃
Max temperature difference:110℃
Max allowable working pressure:
Normal pressure: 0.1MPA~0.15MPA
Negative pressure: 0.1MPA
Accept customized design
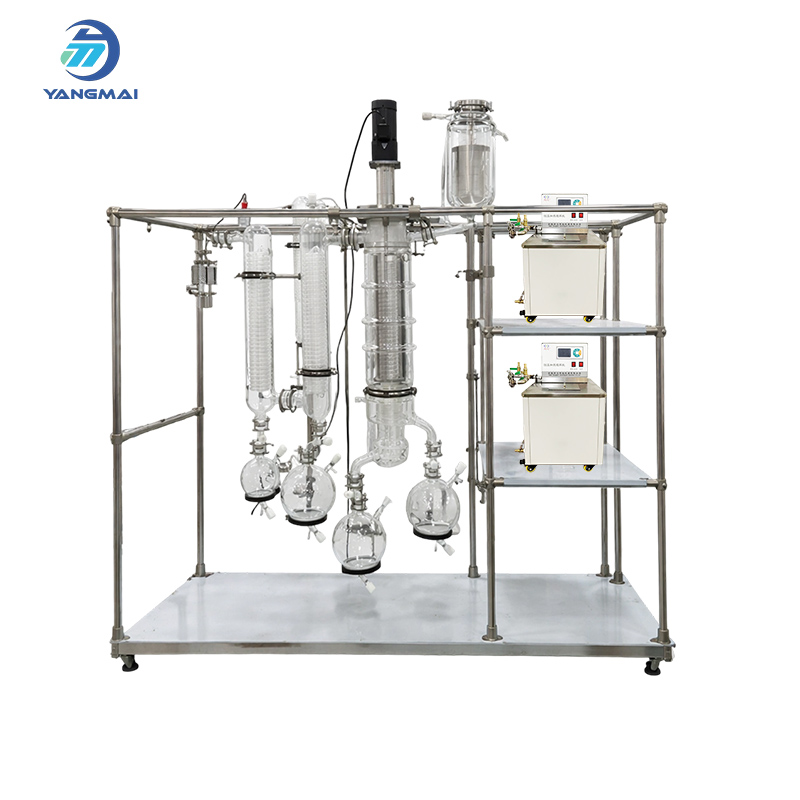
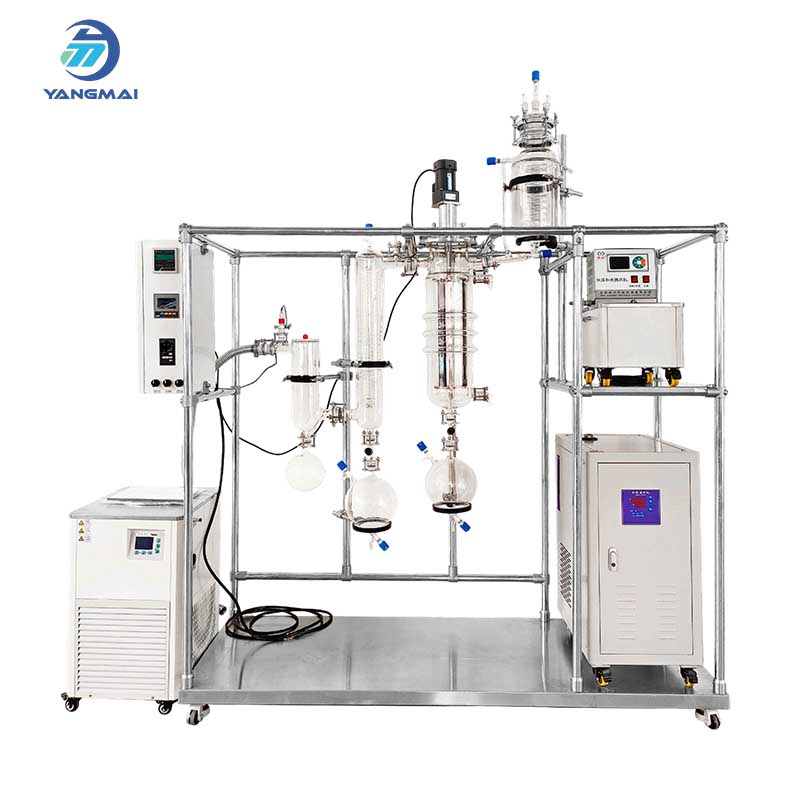
The glass molecular distillation enables gentle separation of high-boiling or heat-sensitive compounds under high vacuum. It's ideal for pharmaceutical, plant oil, and fine chemical purification.
Feature:
High Evaporation Efficiency
Short Residence Time
Strong Corrosion Resistance
Visual Process Monitoring
Accpet Customized Design
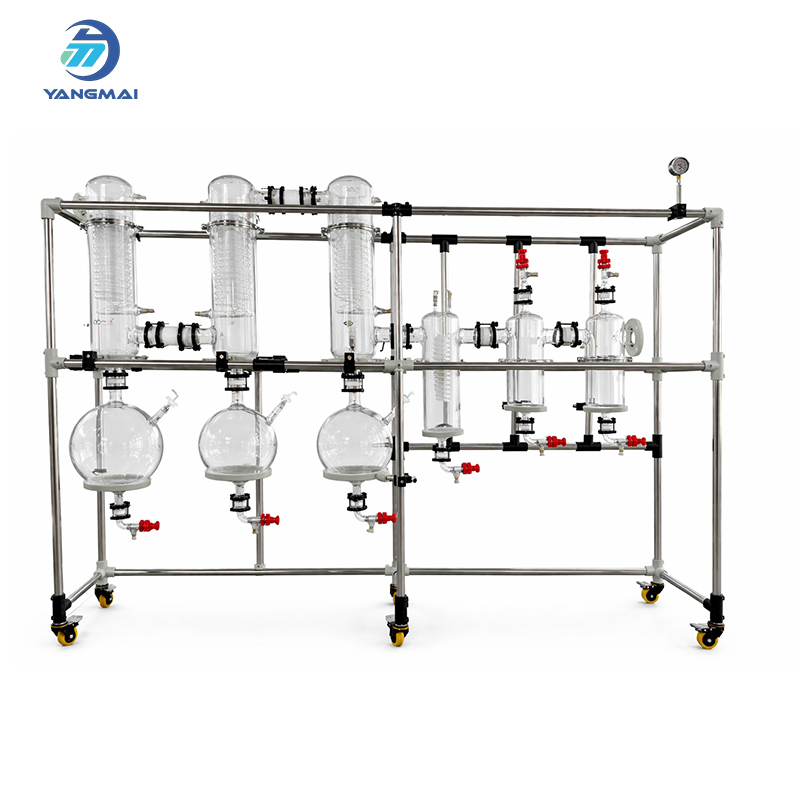
The glass exhaust gas absorption device efficiently removes harmful emissions from chemical reactions, ensuring a clean and safe lab environment. Designed for laboratory and industrial use, it neutralizes acid gases and vapors from exhaust systems.
Feature:
High Corrosion Resistance
Customizable Reactor Interface
Transparent Glass Structure
Precise Flow Regulation
Accept Customized Design
The 10 Square Meter Glass Falling Film Evaporator is ideal for visible and controllable chemical reactions at lab or pilot scale. Perfect for extraction, alkylation, and organic compound synthesis.
Feature:
Large Unit Heating Area
Short Solution Residence Time
High Heat Transfer And Evaporation Efficiency
Transparency And Clarity
Corrosion Resistance
The glass off-gas absorption system is designed to treat harmful reaction exhaust generated during laboratory chemical processes. It efficiently absorbs acidic and corrosive gases before they are released into the environment.
Feature:
High Corrosion Resistance
Customizable Reactor Interface
Transparent Glass Structure
Precise Flow Regulation
Accept Customized Design
200L double-layer glass reactor with an integrated heating and cooling circulator provides stable temperature control for large-scale chemical synthesis, distillation, and extraction processes in laboratories and industrial settings.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Wide temperature range: -100℃~300℃
Transparent and easy to observe
Accept customized design
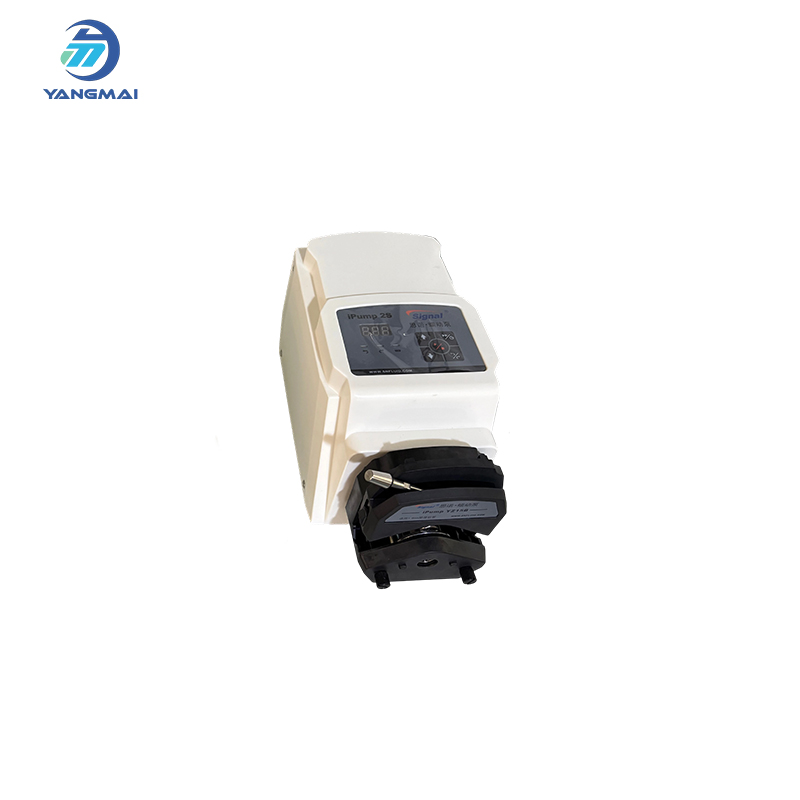
The peristaltic pump provides accurate, contamination-free liquid transfer for laboratory and industrial applications, ideal for chemical dosing and continuous flow systems.
Feature:
Higher Metering Precision
High Flow Rate
Energy Saving Design
The glass coil condenser provides efficient, corrosion-resistant heat transfer for high-purity applications such as solvent condensation and acid recovery.
Feature:
Acid and alkali resistant(Except hydrofluoric acid, phosphoric acid, and concentrated alkali solution at high temperature)
Max operation temperature range: 200℃
Max temperature difference:120℃
Max allowable working pressure:
Normal pressure: 0.1MPA~0.15MPA
Negative pressure: 0.1MPA
Accept customized design