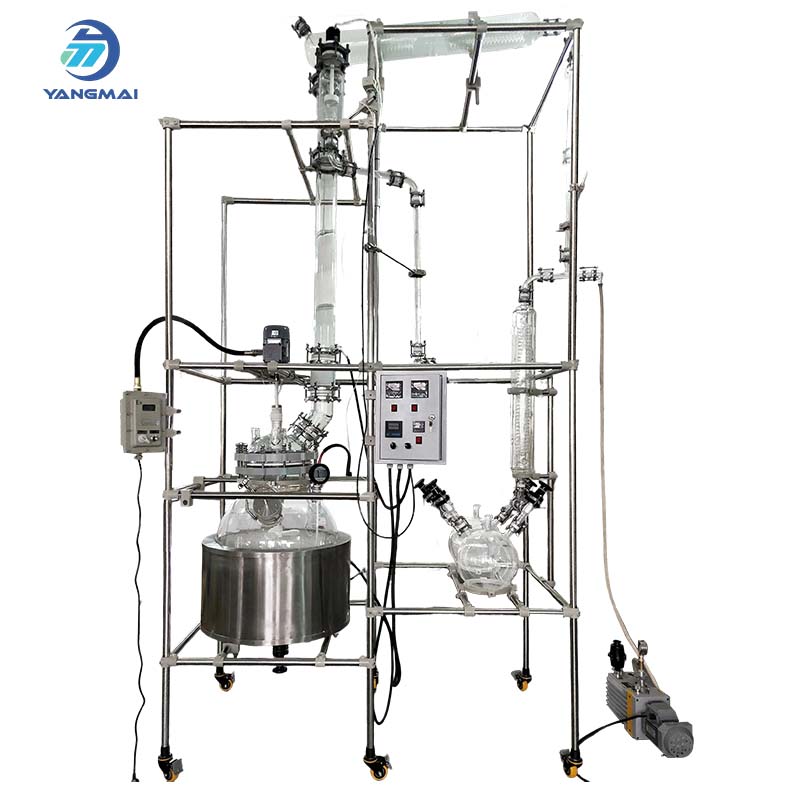
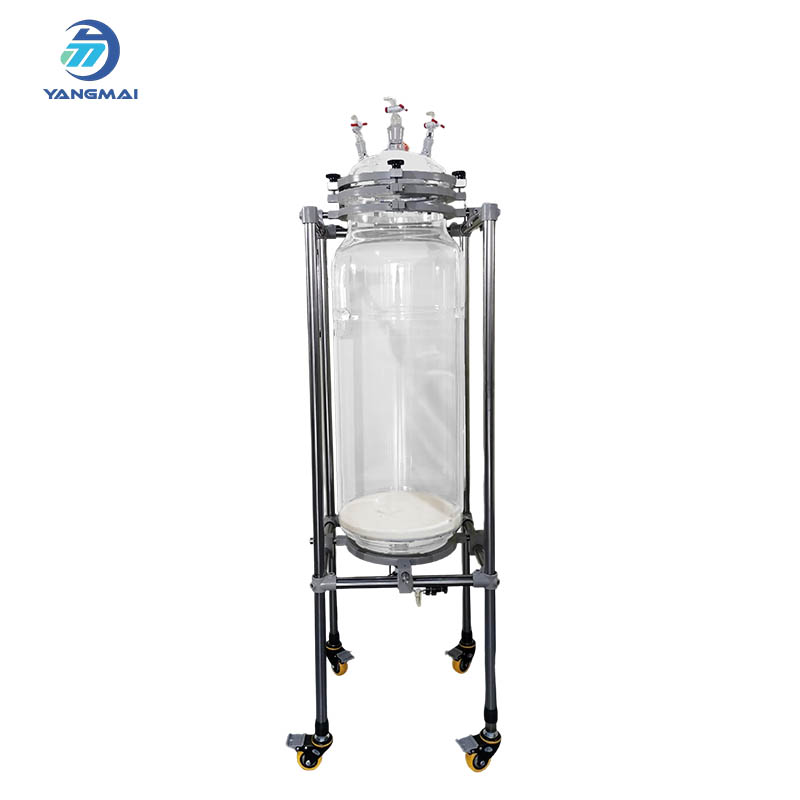
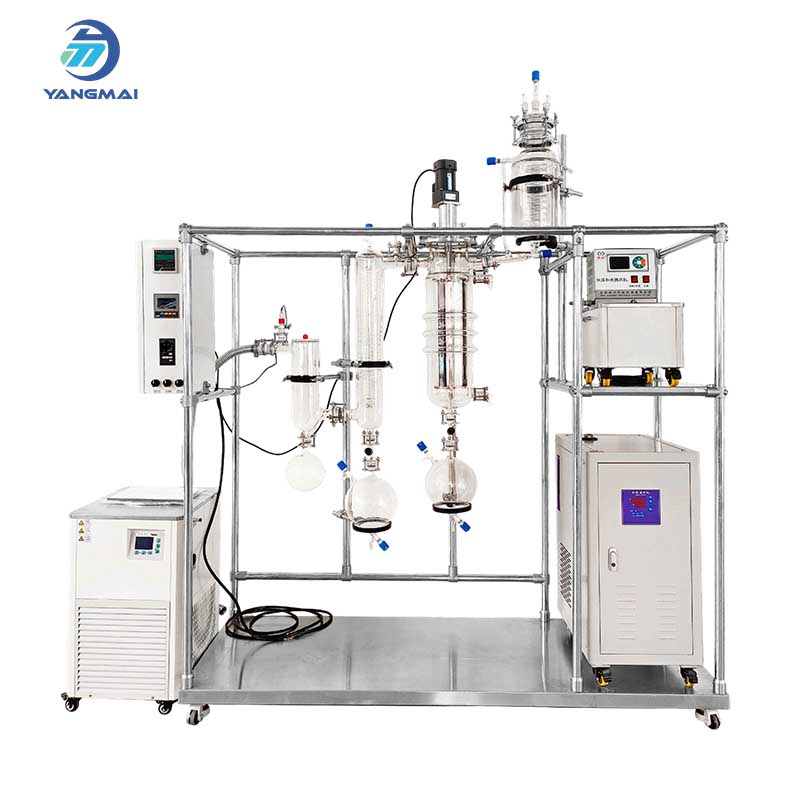
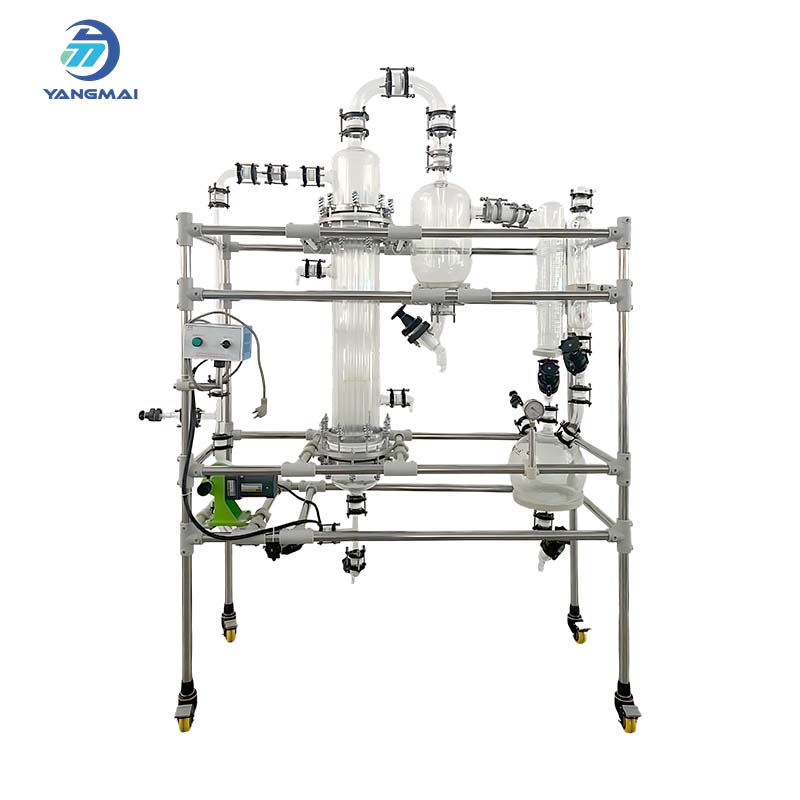
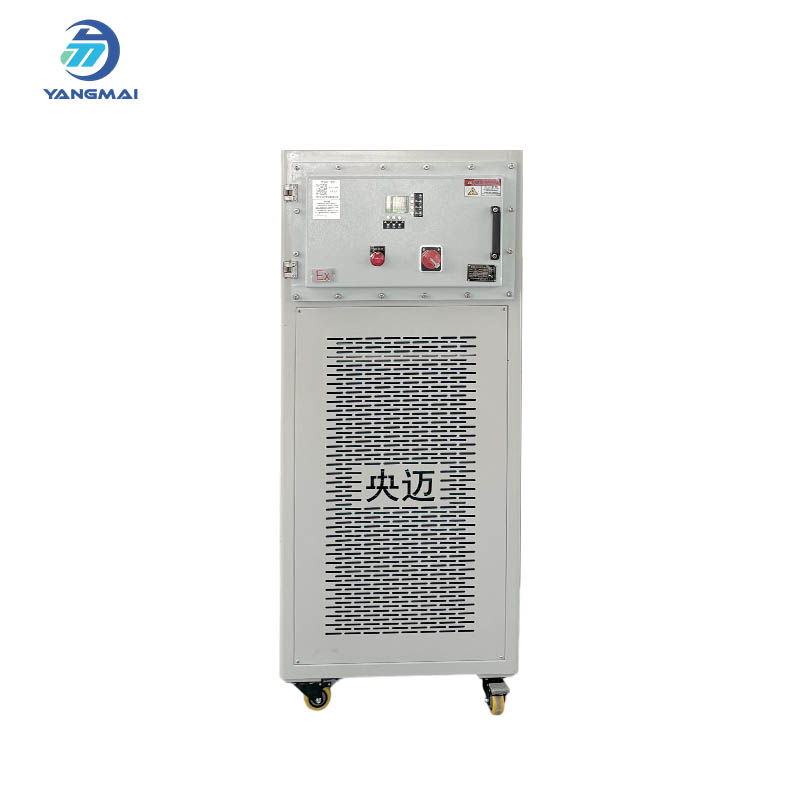
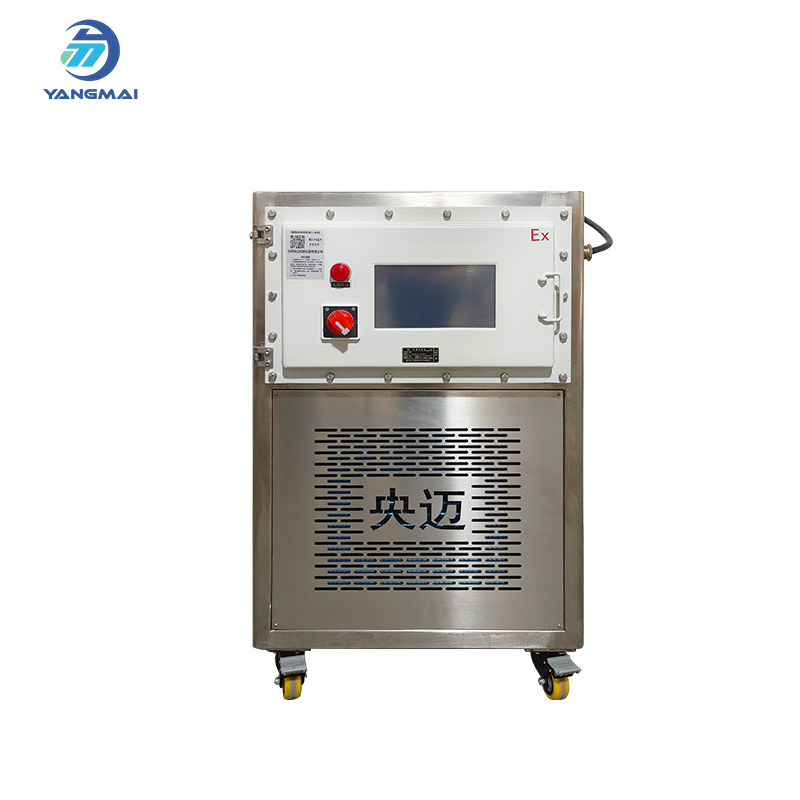
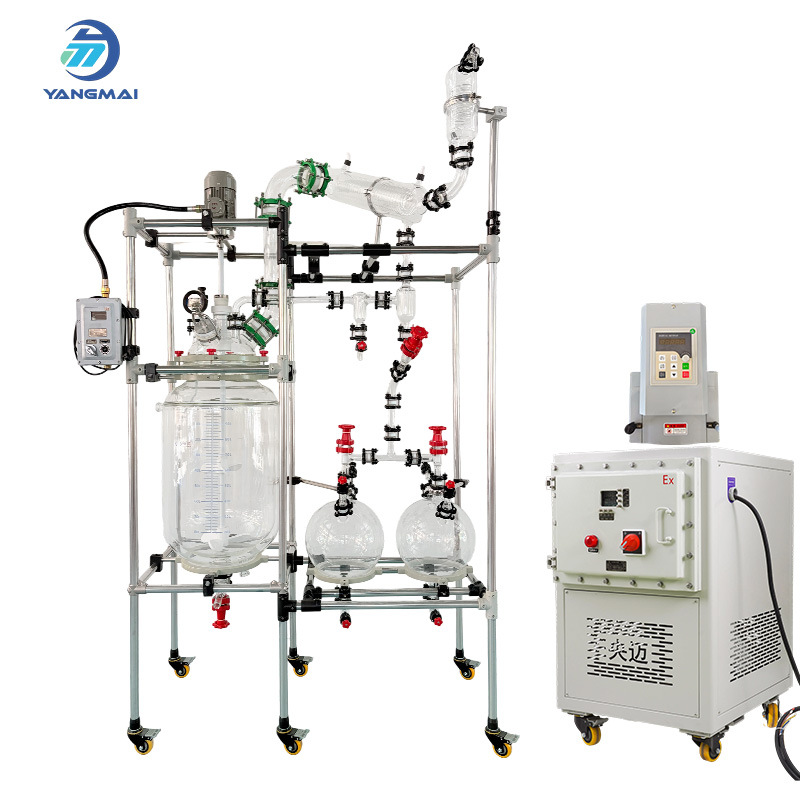
100L Glass Distillation Reactor features a jacketed vessel and built-in condenser, the reactor enables efficient and controlled distillation of complex chemical mixtures.
Excellent Chemical Resistance – Resistant to most acids, alkalis, and organic solvents.
Wide Temperature Range – Operating range: -100°C to +300°C.
Large Reaction Capacity – Suitable for laboratory and pilot-scale applications.
Reliable Stirring System – Ensures stable and uniform mixing.
Customizable Design – Configuration can be tailored to process requirements.